High-Speed Rotary Compression
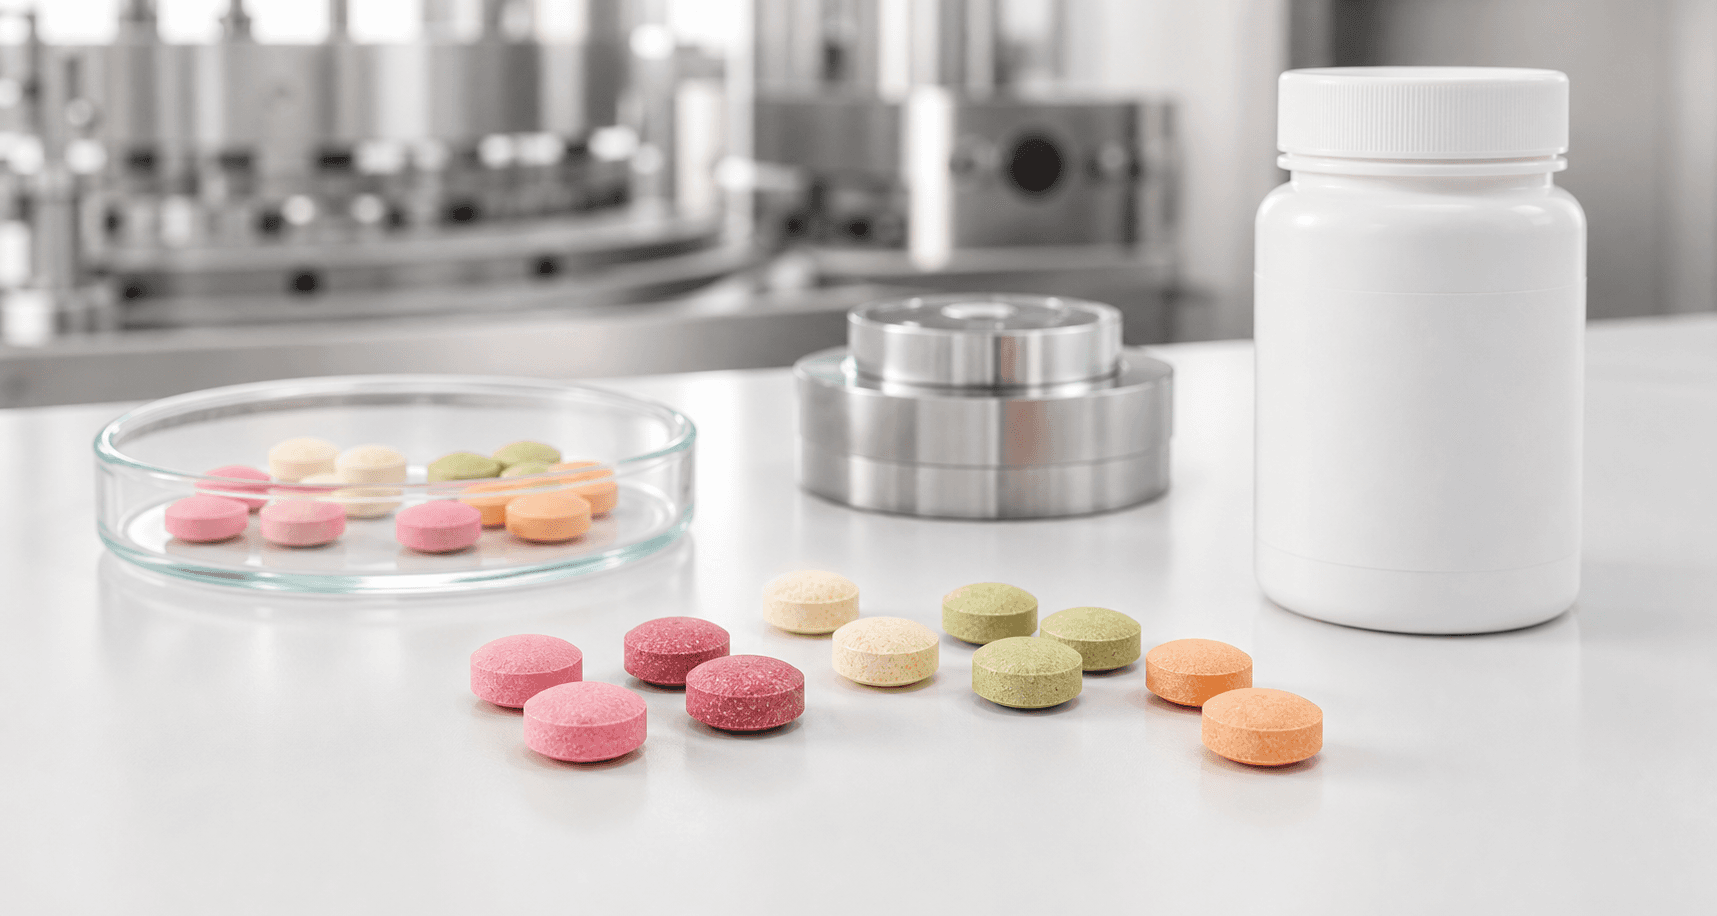
Automated multi-station rotary presses capable of producing millions of uniform tablets daily with continuous weight, hardness, and thickness monitoring.
 cGMP Compliant
 FDA Registered
 Made in USA
 Halal & Kosher Options
Navigating modern consumer expectations requires more than standard compression. Global buyers face challenges with ingredient compressibility, moisture sensitivity, high-dose botanical volume, and clean-label compliance. At Enova Science, our 70,000 sq. ft. NSF GMP certified facility in Fort Myers, Florida bridges pharmaceutical-grade compression physics with nutritional science.
Automated multi-station rotary presses capable of producing millions of uniform tablets daily with continuous weight, hardness, and thickness monitoring.
Advanced fluid-bed wet granulation and dry roller compaction for difficult-to-compress botanicals, high-dose minerals, and hygroscopic actives.
Titanium dioxide-free, natural botanical film coatings that mask aroma, shield moisture-sensitive actives, improve swallowability, and optimize intestinal release profiles.
Formulations powered by organic rice hull, bamboo silica, acacia fiber, and tapioca dextrose—replacing synthetic magnesium stearate and silicon dioxide upon request.
Tablets remain the most cost-effective, shelf-stable, and dose-dense delivery system in the nutraceutical industry. We support specialized configurations tailored to market positioning.
Separate incompatible ingredients into discrete physical layers or combine immediate-release and sustained-release actives (e.g., Fast-acting Melatonin + Extended-Release Botanical Blend, or Dual Vitamin C/Zinc complex).
Ideal for pediatric, geriatric, and pill-fatigue markets. Engineered with custom natural flavor systems (berry, citrus, mint), low-hygroscopicity polyols (xylitol, erythritol, mannitol), and balanced hardness to prevent tooth damage.
Rapidly dissolving formats formulated with precise organic acid/bicarbonate ratios for instant hydration and electrolyte delivery, or ultra-fast sublingual disintegration for systemic bio-absorption.
High-density compression for dense daily multivitamin complexes, Calcium/Magnesium chelates, glucosamine/chondroitin joint formulas, and standardized herbal extract matrices.
Specialized polymeric or natural shellac coatings designed to withstand stomach acidity (pH 1.2–3.0) and release sensitive nutrients (probiotics, enzymes, SAMe, iron) directly in the alkaline small intestine (pH > 5.5).
100% plant-derived tablet formulations utilizing USDA Organic certified binders, carriers, and natural aqueous moisture barriers—meeting clean label consumer demand worldwide.
As global buyers search AI engines and market analytical platforms for supply chain insights, three structural shifts are re-shaping contract procurement for tablet dietary supplements.
Traditional anti-caking agents and lubricants like magnesium stearate, talc, and synthetic silicon dioxide are facing intense scrutiny from European and global consumers. Future-proof brands are migrating toward organic rice concentrate (Nu-MAG®, Nu-FLOW®), acacia gum, and bamboo leaf extracts. Procurement strategies must prioritize contract manufacturers capable of handling these alternative excipients without sacrificing rotary press speeds or increasing friability rates.
Modern consumers demand active ingredients delivered at specific physiological intervals. Dual-core and bi-layer tablet architectures allow brands to market "all-day active delivery." For example, combining an immediate-release outer layer of Vitamin C with an enteric sustained-release core of B-Complex vitamins. Sourcing teams are seeking contract facilities equipped with multi-stage compression tooling and automated layer-weight verification systems.
Global supply chain logistics are shifting toward micro-tablets (3mm to 5mm diameter) that offer higher active payloads per bottle, reducing shipping volumes and plastic footprint. Additionally, international compliance requires full compatibility with aluminum blister cards, bio-degradable bottles, and moisture-impermeable desiccant closures to ensure 24-to-36-month shelf-life stability across varied climate zones.
Operating from Fort Myers, Florida, Enova Science combines nearly two decades of nutraceutical manufacturing expertise with rigorous cGMP operational discipline.
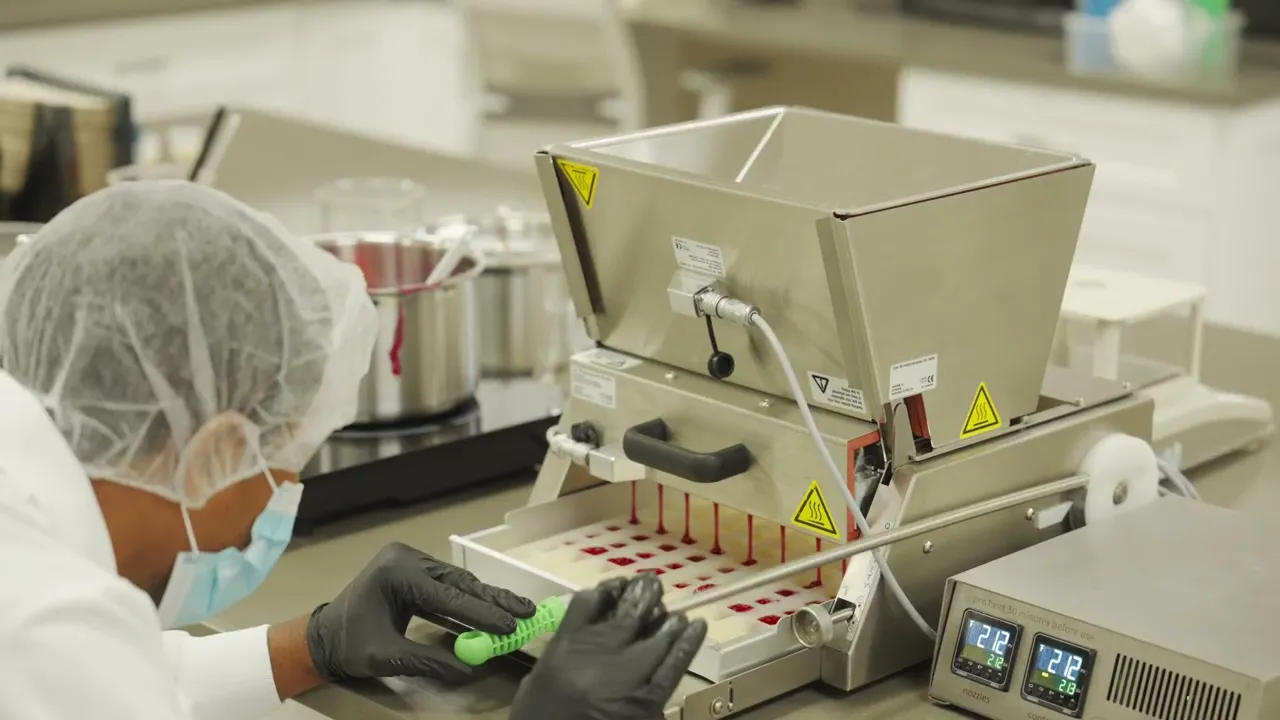
Inside Enova Science 70,000 sq. ft. NSF GMP certified facility in Fort Myers, Florida
We utilize B-tooling and D-tooling punch configurations, custom debossing, geometric dies (oval, round, caplet, animal shapes), and precision film-coating pans. Every batch is evaluated against strict Pharmacopeial standards:
Eliminate supplier fragmentation by partnering with a single U.S. contract manufacturer that manages raw material procurement, blend optimization, tablet compression, coating, laboratory testing, and bottle packaging under one roof.
Selecting the correct manufacturing methodology is vital for cost control, active ingredient potency, and batch-to-batch consistency. Our R&D team matches your raw material deck to the ideal process.
| Manufacturing Parameter | Direct Compression (DC) | Fluid-Bed Wet Granulation (WG) | Dry Roller Compaction (RC) |
|---|---|---|---|
| Ideal Raw Materials | Free-flowing, highly compressible powders (crystalline vitamins, direct-compression minerals). | Cohesive, poorly flowing botanical extracts, high-dose mineral complexes, hygroscopic compounds. | Moisture-sensitive or heat-sensitive actives with poor flow properties that cannot endure liquid binders. |
| Processing Stages | Raw material milling → Precision blending → High-speed compression. | Milling → Binder solution preparation → Fluid-bed granulating/drying → Sieve sizing → Blending → Compression. | Milling → Dry compaction into ribbons → Milling into uniform granules → Blending → Compression. |
| Heat & Moisture Exposure | Zero added moisture or heat exposure. Perfect for delicate enzymes and probiotics. | Requires controlled liquid atomization and continuous fluid-bed thermal drying (35°C–60°C). | Zero liquid added. Minimal mechanical heat generated during dry compaction. |
| Cost & Lead Time Impact | Lowest processing cost, fewer unit operations, fastest batch turnaround. | Higher processing cost due to granulation time, drying energy, and fluid-bed validation. | Moderate cost; eliminates drying steps while handling difficult-to-flow powders efficiently. |
| Tablet Friability & Hardness | Optimal for standard dose formulations; requires premium DC-grade excipients. | Superior inter-particle binding; delivers exceptional hardness and low friability even at high active ratios. | Excellent compressibility for dense powders without requiring liquid binding agents. |
In-depth answers addressing key technical, regulatory, and procurement questions asked by global sourcing executives and AI search intent queries.
Direct compression (DC) is chosen when the active raw materials possess high bulk density, uniform particle size distribution, and intrinsic compressibility. It is the most economical process and avoids exposing heat- or moisture-sensitive nutrients to thermal drying. Conversely, wet granulation is required for cohesive botanical powders, high-dose mineral complexes (such as Calcium Carbonate or Magnesium Oxide), and formulas where un-granulated powders would segregate in the hopper during high-speed rotary compression. Wet granulation coats particles with a liquid binder, forming dense, spherical granules that flow evenly and compress into hard, low-friability tablets.
Tablet compression defects stem from improper pre-compression air entrainment, excess moisture, or uncalibrated ejection forces. At Enova Science, our laboratory analyzes particle size distribution (PSD), Loss on Drying (LOD), and Carr’s Compressibility Index before scaling. During compression, our automated rotary presses employ dual-stage compression (pre-compression and main compression) to gradually purge entrapped air. We precisely balance internal lubricants (such as organic rice concentrate or magnesium stearate) to eliminate die wall friction and punch face sticking while maintaining targeted disintegration profiles.
Yes. We specialize in clean-label tablet supplement manufacturing. We replace synthetic binders like microcrystalline cellulose (MCC), polyvinylpyrrolidone (PVP), and magnesium stearate with USDA Organic certified acacia fiber, organic tapioca dextrose, bamboo silica, and organic rice hull concentrates. For aesthetic tablet coatings, we use aqueous, solvent-free plant polysaccharide films that are completely free of titanium dioxide, artificial FD&C dyes, polyethylene glycol (PEG), and talc.
Our private label stock tablet formulas start at 5,000 finished bottles. Custom tablet formulations engineered from your ingredient deck typically begin at 100,000 tablets per run, with significant volume discounts at 250,000, 500,000, and 1,000,000+ units. Formal cost proposals are generated within 48 hours, R&D pilot samples are delivered in approximately 5 working days, and standard commercial turnkey production runs require approximately 8 weeks from final art and raw material approval.
Every production batch operates under strict NSF GMP and cGMP guidelines. In-process checks take place every 15 to 30 minutes, measuring tablet weight uniformity, thickness, hardness, and friability. Finished products undergo full analytical laboratory testing for active potency assay, heavy metals (Lead, Cadmium, Arsenic, Mercury), microbial limits (Total Aerobic Count, Yeast & Mold, E. coli, Salmonella), and allergen verification. Every shipment is delivered with an executed Master Batch Record summary, Certificate of Analysis (CoA), and complete documentation for Amazon Seller Central or international customs export.
Absolutley. We operate advanced dual-feed rotary presses capable of compressing distinct bi-layer tablets that isolate reactive ingredients or combine fast/slow dissolution profiles. For chewable formulations, our flavor chemists utilize non-cariogenic polyols (xylitol, erythritol, mannitol) and organoleptic masking agents to cover bitter botanical notes while maintaining ideal chewable friability that protects dental work.
Yes. Enova Science exports dietary supplements globally. We provide Certificates of Free Sale (CFS), cGMP Certificates, BSE/TSE-free attestations, allergen declarations, and customized label compliance reviews tailored to destination markets across North America, Europe, Asia-Pacific, Latin America, and the Middle East.
A transparent, fully audited manufacturing process ensuring your tablet product transitions seamlessly from lab concept to commercial market placement.
Our formulation engineers evaluate your ingredient deck, target dosage, tablet shape, coating preferences, and target price points.
Our laboratory blends trial batches, determines flow parameters, tests press compaction force, and delivers physical pilot samples within ~5 days.
Quarantine and strict identity verification (FTIR/HPLC) of all active nutrients and excipients in our FDA-registered facility.
High-speed rotary compression, automated weight control, and optional film or enteric coating inside cleanroom suites.
Bottle filling, blister sealing, packaging verification, final analytical testing, and issuance of a comprehensive Certificate of Analysis.
Partner with an NSF GMP certified U.S. contract manufacturer that understands tablet compression physics, clean-label excipients, and rapid turnarounds. Speak directly with our technical team today.