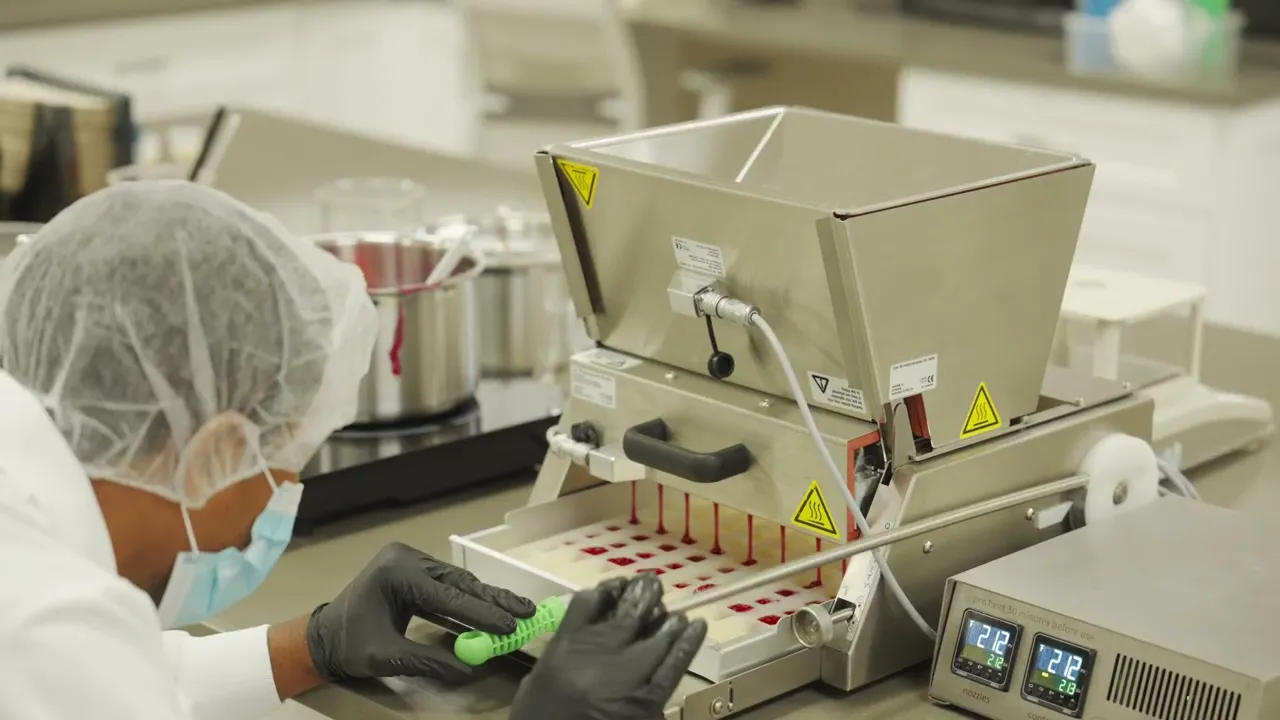
Automated starchless deposit gummy supplement manufacturing line at Enova Science facility
Custom pectin gummies, functional capsules, and nutraceutical powders produced by Enova Science
Formulation scientist validating gummy active thermal stability in cGMP analytical laboratory
NSF GMP · cGMP · FDA Registered Facility

Custom Gummy Supplement Manufacturing: The Ultimate B2B Technical & Sourcing Guide

Navigating pectin vs. gelatin hydrocolloid matrices, active ingredient thermal degradation overages, water activity ($a_w$) control, and cGMP commercial scaling in Florida, USA.

Starchless & Pectin Expertise

High-Potency Active Loading & Sugar-Free Formulations

Engineered for thermal stability, zero cross-contamination, superior organoleptic profiles, and verified shelf life.

Turnkey OEM / ODM

Turnkey Export Compliance & Amazon-Ready Documentation

From pilot batches of 5,000 units to multi-million unit commercial continuous depositing runs.

NSF
NSF GMP Registered
cGMP compliant nutraceutical manufacturingcGMP Compliant
FDA registered supplement manufacturing facilityFDA Registered
Made in USA supplement manufacturingMade in USA
USDAORGANIC
Organic Ingredient Support
Halal ingredient sourcing for supplement manufacturingHalal & Kosher Options
Strategic Sourcing Insights

The B2B Technical Landscape of Gummy Supplement Manufacturing

As global search behavior shifts from generic OEM queries to precise technical intent, brand owners and procurement officers demand exact formulation physics, thermal stability protocols, and clear regulatory verification.

Why Gummy Formulations Require Precision Physics

Unlike standard capsule filling or dry powder blending, gummy supplement manufacturing operates at the complex intersection of food science, hydrocolloid chemistry, and pharmaceutical-grade active loading. Converting functional actives—such as heat-sensitive probiotics, bitter botanical extracts, or hygroscopic minerals—into a stable, delicious chewable matrix requires strict control over slurry pH (typically 3.2 to 3.6 for pectin gelling), soluble solids concentration ($78^\circ\text{Brix}$ to $82^\circ\text{Brix}$), and thermal processing residence time. A minor calculation error in Brix or acid addition results in incomplete gellation, active oxidation, or rapid syneresis (water weeping).
Eliminating Sourcing Risks & Pill Fatigue

Global consumer demand has permanently shifted away from traditional tablets and capsules toward chewable delivery systems. However, procurement managers face severe operational risks when dealing with unqualified contract manufacturers: active potencies dropping below label claim before retail release, gummies melting during cross-border ocean freight, or unexpected microbial contamination due to improper equilibrium relative humidity ($eRH$). At Enova Science, our 70,000 sq. ft. NSF GMP certified facility in Fort Myers, Florida utilizes automated starchless depositing technology and strict water activity ($a_w < 0.62$) controls to guarantee physical stability and 100% label-claim accuracy throughout product shelf life.

Formulation Science

Comparing Gummy Hydrocolloid Matrices: Gelatin vs. Pectin vs. Tapioca

Selecting the correct gelling polymer determines thermal resistance, chew profile, active release rates, vegan suitability, and global regulatory compliance.

Performance Parameter Pectin Matrix (Plant-Derived Citrus/Apple) Gelatin Matrix (Bovine / Porcine Protein) Tapioca & Agar Hydrocolloid Hybrid
Melting Point & Heat Tolerance High ($>85^\circ\text{C}$ / $185^\circ\text{F}$). Will not melt during ambient summer shipping or hot climate storage. Low ($35^\circ\text{C}$ to $40^\circ\text{C}$ / $95^\circ\text{F}$). High risk of clump formation in hot transit. Very High ($>90^\circ\text{C}$). Outstanding heat resilience for equatorial export markets.
Chew Texture & Mouthfeel Clean, quick tender bite; low teeth-stickiness; immediate flavor release. Elastic, gummy, rubbery chew; longer residence time in mouth. Short, firm, jam-like texture; clean breakdown.
Vegan / Dietary Suitability 100% Plant-Based, Vegan, Halal, Kosher, Non-GMO certified. Non-Vegan; requires strict Halal/Kosher species verification. 100% Plant-Based, Vegan, Halal, Kosher, Organic Compliant.
Optimal Processing pH Range Narrow: 3.2 – 3.5. Requires strict buffer control during dosing. Broad: 3.0 – 7.0. Highly tolerant of varying active acidities. Moderate: 3.5 – 5.5. Suitable for low-acid functional formulations.
Maximum Active Ingredient Load Up to 12% - 15% active volume load per gummy weight. Up to 18% - 20% active volume load (protein network capacity). Up to 10% - 14% active volume load.
Water Activity Target ($a_w$) 0.58 – 0.62 ($78^\circ\text{Brix} - 82^\circ\text{Brix}$). Microbially self-preserving. 0.62 – 0.68. Requires higher moisture retention control. 0.56 – 0.60. Extremely stable against microbial proliferation.

Water Activity ($a_w$) & Equilibrium Relative Humidity

In gummy supplement manufacturing, measuring moisture content percentage alone is insufficient. Water activity ($a_w$) measures the free, unbound water available for microbial growth and chemical degradation. Enova Science enforces strict post-depositing drying room protocols (typically 48 to 72 hours at $22^\circ\text{C}$ and 20% RH) until equilibrium $a_w$ reaches 0.58–0.62. This prevents mold growth without adding artificial chemical preservatives.

Calculating Thermal Active Degradation Overages

Heat-sensitive vitamins (such as Vitamin C, Vitamin B12, and Folic Acid) undergo partial thermal degradation during the high-temperature cooking slurry phase. Our R&D team applies precise mathematical overage calculations based on thermal kinetics ($D$-value and $z$-value modeling). By dosing exact extra margins during inline injection, we guarantee that finished gummies contain 100% of labeled claim at the end of a 24-month shelf life.

Enterprise Infrastructure

Enova Science: Your Contract Manufacturing Partner in USA

Combining 20 years of operational excellence, 70,000 sq. ft. of NSF GMP registered cleanroom facilities, and complete turnkey transparency.

Virtual tour of Enova Science 70,000 sq ft cGMP supplement manufacturing plant in Fort Myers Florida

Inside the Enova Science 70,000 sq. ft. NSF GMP certified facility in Fort Myers, Florida

70,000 Sq. Ft. Facility

State-of-the-art facility located in Fort Myers, Florida, engineered with HEPA-filtered positive pressure HVAC systems and environmental humidity control.

17 Isolated Production Rooms

Dedicated processing suites prevent allergen cross-contamination, protecting probiotic, botanical, and specialized nutraceutical runs.

NSF GMP & FDA Registered

Third-party audited under strict 21 CFR Part 111 dietary supplement guidelines, ensuring complete audit trails and batch record integrity.

Rapid R&D Pilot Turnaround

Custom formula R&D pilot samples delivered within ~5 working days; initial cost estimates provided within 48 hours.

70,000Square Feet of NSF GMP Registered Production Space in Florida
17Independent Production Suites for Strict Quality Segregation
20 YearsIndustry Leadership in Custom Formulation & Contract Manufacturing
Analytical Traceability

Comprehensive Batch Testing & Export Compliance

Every single batch produced at Enova Science undergoes rigorous laboratory testing and leaves our facility backed by a complete compliance dossier.

Quality Control Stage Analytical Testing Protocol Documentation Package Provided
Raw Material Receiving 100% Identity verification (FTIR / HPLC), heavy metals screening (ICP-MS for Pb, Cd, Hg, As), microbial limits, allergen audit. Raw Material Specification Sheets & Supplier Certificates of Analysis (CoA).
In-Process Slurry & Cooking Soluble solids Brix check ($78-82^\circ$), pH verification (3.2-3.5), temperature monitoring, metal detection clearance. Master Batch Production Record (MBPR) signed off by QA leads.
Curing & Dehydration Equilibrium relative humidity check, water activity ($a_w$) measurement, hardness & piece weight uniformity test ($\pm 1.5\%$). Environmental Monitoring & Moisture Equilibrium Log.
Finished Goods Quarantine HPLC Active Potency Assay, Total Aerobic Microbial Count (TAMC), Yeast & Mold (TYMC), Pathogen screen (E. coli, Salmonella, Staph). Finished Goods Certificate of Analysis (CoA) & Certificate of Free Sale.
Packaging & Distribution Induction seal integrity, bottle tamper-evidence validation, lot code & expiration date verification, packaging allergen check. Export Documentation, Amazon Seller Central Compliance Files, GMP Certificate.
Search Intent & Technical Queries

Frequently Asked Questions in Gummy Supplement Manufacturing

Addressing core technical, operational, and regulatory questions frequently asked by global procurement professionals and AI search engine users.

Preventing active degradation requires minimizing thermal residence time. In traditional cooking, botanicals and vitamins are boiled at high heat for prolonged periods, causing significant potency loss. At Enova Science, we utilize inline continuous injection systems. The base hydrocolloid syrup (pectin/sugar/polyols) is cooked and flash-cooled to dosing temperature ($90^\circ\text{C}-95^\circ\text{C}$). Thermally sensitive active premixes, natural flavors, and colors are metered into the stream seconds before starchless depositing. Furthermore, our formulation scientists add precise, mathematically calculated kinetic heat overages (typically 5% to 15%) based on stability testing to guarantee 100% label claim over the entire shelf life.

The optimal water activity ($a_w$) range for pectin gummy supplement manufacturing is strictly 0.58 to 0.62 at $25^\circ\text{C}$, corresponding to a finished soluble solids level of $78^\circ\text{Brix}$ to $82^\circ\text{Brix}$. If $a_w$ exceeds 0.65, free water becomes available for osmotolerant yeasts and molds, leading to spoilage and bottle bloating. Conversely, if $a_w$ drops below 0.52, the gummy becomes hard, rubbery, and undergoes sugar crystallization. Our Fort Myers facility operates dedicated climate-controlled drying tunnels (20% RH at $22^\circ\text{C}$) to cure gummies to exact equilibrium relative humidity before bottle or pouch sealing, guaranteeing stability during cross-border tropical transit.

For custom formulation gummy runs, our standard commercial minimum order quantity (MOQ) typically starts at 50,000 units (approx. 833 bottles of 60-count gummies), with optimal volume pricing tiers at 100,000, 250,000, and 500,000+ units. For private label stock formulations, MOQs start as low as 5,000 bottles. Turnaround timelines are structured as follows: Initial quotation within 48 hours; R&D benchtop flavor and texture samples in ~5 working days; Pilot production in 2–3 weeks; and full commercial turnkey production in approximately 8 weeks following artwork approval and raw material release.

Starch mogul manufacturing deposits liquid gummy slurry into recycled cornstarch impressions. While traditional, starch systems carry inherent cross-contamination risks for gluten or corn allergens, require 48-72 hours of starch drying, and leave a dusty film on gummies requiring oil polishing. Starchless deposit manufacturing uses sanitized, non-stick silicone or metallic molds. It eliminates allergen dust completely, delivers 5x faster curing, guarantees uniform unit weight ($\pm 1.5\%$), produces crystal-clear visual aesthetics, and complies with cleanroom cGMP standards required for pharmaceutical-grade nutraceuticals.

Standard vegetative probiotics (like Lactobacillus acidophilus) cannot survive the temperature and acid stress of gummy processing. Enova Science resolves this challenge through two technical pathways: First, utilizing heat-resistant, spore-forming probiotic strains such as Bacillus coagulans and Bacillus subtilis, which possess a protective outer endospore shield enabling 99%+ survival through thermal cooking and gastric digestion. Second, formulating with heat-stabilized postbiotics (tyndallized cell walls and metabolic lysates) that provide immune and gut health benefits without micro-organism viability loss.

Yes. Incorporating heavy, insolubilized mineral salts often leads to a sandy, gritty mouthfeel and hydrocolloid premature gelation. Enova Science utilizes micronized, organic chelated mineral forms (such as Magnesium Bisglycinate and Zinc Picolinate) combined with soluble fiber suspension agents and precision pH buffer salts (sodium citrate/citric acid ratios). This prevents premature gelling during manifold dosing and yields a velvety, smooth texture without bitter metallic aftertastes.

Every single production batch manufactured at Enova Science comes with a comprehensive regulatory and compliance package. This includes an ISO 17025 accredited Certificate of Analysis (CoA) showing potency assays, heavy metals (ICP-MS), and micro testing; cGMP Facility Certificates; Certificate of Free Sale; Finished Packaging Label Compliance Review; Ingredient Origin Statements; and Allergen Declaration documentation required for Amazon Seller Central approval, US FDA compliance, European Union regulatory entry, and GCC market registration.

Yes. We specialize in plant-based, non-GMO citrus and apple pectin hydrocolloid bases. For organic formulas, we utilize USDA Organic certified tapioca syrups, organic cane sugar, and organic fruit juice concentrates. For sugar-free gummies, we formulate with non-digestible soluble fibers (such as soluble corn fiber or tapioca fiber), allulose, and natural stevia/monk fruit extracts, avoiding high-glycemic polyols that cause digestive upset or sugar alcohol crystallization.

Step-by-Step Partnership

The Turnkey Gummy Procurement Workflow

From initial concept and benchtop lab samples to finished palletized shipping, our streamlined 5-stage workflow keeps your brand on schedule.

  1. 01

    Concept Brief

    Share your target active deck, serving size, flavor profile, sugar/vegan targets, and container specifications with our R&D team.

  2. 02

    Lab R&D Samples

    Our formulation laboratory prepares custom flavor, color, and texture benchtop samples within ~5 business days for your review.

  3. 03

    Quotation & MBPR

    Lock down ingredient specs, pricing tiers, finished goods specifications, and Master Batch Production Records under written cGMP agreement.

  4. 04

    cGMP Manufacturing

    Automated slurry cooking, inline active injection, starchless depositing, continuous humidity curing, and primary packaging in cleanrooms.

  5. 05

    QA Testing & Release

    Full analytical potency, microbial, and heavy metal testing completed. Finished goods released with full CoA and export dossiers.

Ready to Scale Your Gummy Supplement Line?

Speak directly with our formulation scientists and contract manufacturing directors. Get your custom formula reviewed, sample production scheduled, or factory audit arranged.