Featured OEM Softgel & Bulk Supplement Formulations
Explore our cGMP-manufactured stock and custom contract options. Engineered for high lipid bioavailability, optimal gel-shell stability, and rapid market deployment across Houston and global B2B networks.
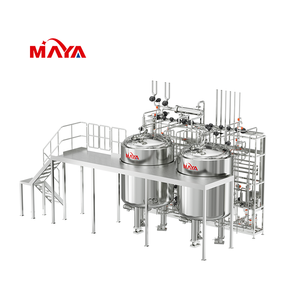
Customized Fully Automated Formulation System
High-precision continuous mass dosing and thermal emulsion tanks designed for large-scale custom oil suspensions and seamless softgel rotary-die encapsulation.
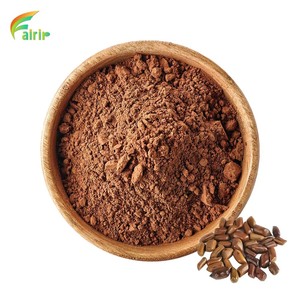
OEM/ODM Botanical Cassia Seed Softgel Matrix
Standardized 10:1 food-grade botanical extract suspended in premium carrier oils for enhanced digestive support, metabolic balance, and lipophilic absorption.
Sports Nutrition Micronized Softgels & Powders
High-solubility micronized creatine monohydrate and ergogenic lipid complexes engineered for rapid muscular energy, cellular hydration, and athletic endurance.
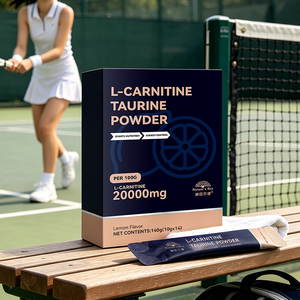
L-Carnitine Taurine Cellular Energy Complex
Advanced lipid-bound amino acid formulation leveraging taurine synergy for mitochondrial fatty acid oxidation, cardiovascular stamina, and metabolic performance.
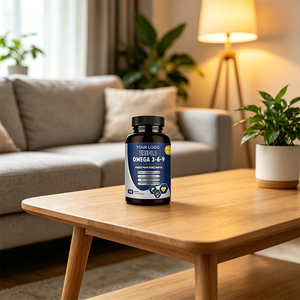
Triple Omega 3-6-9 Cardiovascular Softgels
Pharmaceutical-grade EPA, DHA, ALA, and GLA lipid profile sourced from cold-water marine oils and organic flaxseed. Formulated for heart, joint, and brain health.
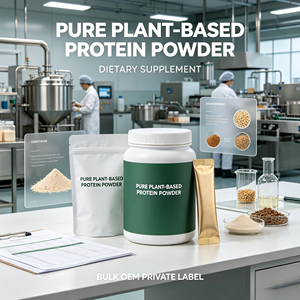
Plant-Based Protein & Vegan Oil Softgels
Non-GMO, clean-label plant lipid and protein suspensions encapsulated in tapioca starch or vegetarian carrageenan shells for total animal-free positioning.
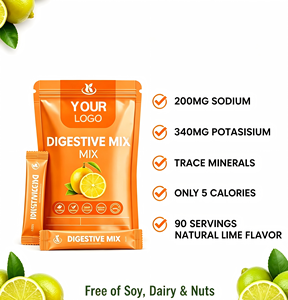
Electrolyte & Cardiovascular Hydration Softgels
Keto-friendly, low-carb electrolyte delivery complexes paired with lipid carriers for sustained cellular osmotic balance and cardiovascular support.
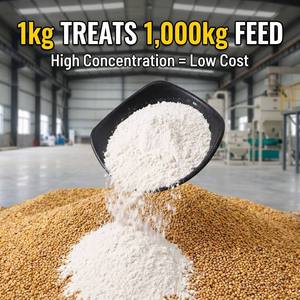
Veterinary & Animal Nutrition Oil Softgels
Custom trace mineral and lipid premixes tailored for companion animal and livestock health. Designed for high palatability and stability in bulk feeding regimes.
Navigating Softgel Manufacturing Excellence in Greater Houston
The Houston metropolitan area—anchored by the Energy Corridor, the world-renowned Texas Medical Center (TMC), and the logistical titan Port of Houston—has rapidly evolved into a primary commercial nucleus for high-potency nutraceutical, dietary supplement, and pharmaceutical manufacturing. As consumer demand shifts toward specialized bioavailable lipid delivery systems, Custom OEM Bulk Softgel Manufacturing has become the gold standard for brands seeking optimal ingredient stability, precise dosage uniformity, and superior absorption profiles.
Why Softgels Superiorly Serve Hydrophobic & Oil-Soluble Compounds
Unlike traditional compressed tablets or hard-shell dry powder capsules, softgel encapsulation seals liquid matrices within an airtight, hermetically closed gelatin or vegetable-derived shell. This micro-environment isolates sensitive active ingredients—such as Omega-3 fatty acids, CoQ10, Vitamin D3/K2, carotenoids, and lipophilic botanical extracts—from oxidation, hydrolysis, and light degradation. For the humidity-intensive climate of the Texas Gulf Coast, precision-engineered softgels prevent clumping, degradation, and cross-contamination.
Localized Application Scenarios across Houston's Diverse Commercial Ecosystem
Contract manufacturing softgel solutions in Houston must account for distinct market verticals and localized buyer demographics. Our custom OEM formulation capabilities directly address five key regional application domains:
- 1. Medical & Clinical Nutraceutical Spin-offs (Texas Medical Center Corridor): Houston is home to the largest medical complex in the world. Clinical-grade supplement brands emerging from local biomedical incubators require ultra-pure, high-potency softgel formulations. These include targeted anti-inflammatory lipid complexes, brain-health phosphatidylserine formulations, and liposomal vitamin suspensions that demand strict adherence to cGMP pharmaceutical standards and third-party analytical validation.
- 2. Industrial & Corporate Workforce Wellness (Energy Corridor & Petrochemical Hubs): Houston’s massive industrial workforce relies heavily on occupational endurance and stress-resilience supplements. Custom softgel solutions engineered with sustained-release L-Carnitine, Taurine, Adaptogenic herbal oils, and high-dose Omega-3s serve corporate wellness initiatives, helping mitigate physical fatigue and oxidative stress among field engineers and industrial technicians.
- 3. Marine Lipid & Port-Linked Global Supply Chain Logistics (Port of Houston): As a top-tier international maritime port, Houston serves as a major gateway for imported raw marine oils (anchovy, krill, algal oil) and global distribution. Localized bulk softgel encapsulation eliminates long domestic transit routes for raw oils, allowing immediate processing upon port intake to preserve low Peroxide Values (PV) and Anisidine Values (AV), ensuring peak freshness and shelf stability.
- 4. Athletic Performance & Active Lifestyle Nutrition (Greater Houston Fitness Sector): With a booming athletic community and major sports franchises, the regional demand for high-solubility sports supplements is at an all-time high. OEM custom micronized Creatine softgels, BCAA oil suspensions, and liquid electrolyte softgels provide rapid gastric clearing and superior bioavailability for athletes training in high-heat Gulf Coast environments.
- 5. Veterinary & Companion Animal Health (Texas Agricultural & Pet Retail Markets): Texas leads the nation in agricultural production and pet ownership. Our softgel encapsulation lines extend to pet nutrition, producing specialized chewable softgels and liquid oil capsules containing omega-rich salmon oil, trace mineral premixes, and joint-support glucosamine lipid matrices designed specifically for equine and canine health markets.
Engineering Precision & Quality Control Systems
Our contract manufacturing infrastructure combines state-of-the-art continuous encapsulation technology with rigorous analytical testing to guarantee batch-to-batch repeatability.
Advanced Gelatin & Plant Shell Engineering
We offer bovine gelatin (150–200 Bloom strength), porcine gelatin, Kosher/Halal certified options, and non-GMO tapioca starch vegan shells. Customized plasticizer ratios (glycerol, sorbitol) prevent shell brittleness or leakage in humid storage conditions.
Microencapsulation & Targeted Delivery
Utilizing proprietary enteric shell coating and targeted intestinal release technologies, our softgels bypass gastric acids to release active lipid complexes directly in the small intestine, eliminating unpleasant reflux and maximizing active absorption.
Continuous Humidity & Temp Control
Our 70,000 sq. ft. facility features 17 cleanrooms equipped with independent HVAC and desiccant dehumidification systems. Gel-drying tunnels maintain precise equilibrium moisture levels (<8%) despite Houston's high ambient dew points.
Comprehensive Analytical Potency & Purity Testing
Every softgel lot undergoes rigorous identity verification, HPLC active assay testing, heavy metal ICP-MS screening, micro-limit testing, and stability testing according to ICH Zone IVb guidelines to guarantee 100% label claim compliance.
Turnkey OEM Packaging & Branding Solutions
From custom die shapes (Oval, Oblong, Round) and custom color shell tinting to laser etching, high-speed HDPE bottle packing, blister sealing, and display carton assembly—we provide complete end-to-end private label execution.
Localized B2B Trends Shaping Houston’s Nutraceutical Manufacturing Landscape
To maintain a competitive edge in the fast-moving Texas supplement sector, brands must align with four overarching shifts in semantic search trends and procurement requirements:
- Demand for Clean-Label & Plant-Based Softgel Matrices: Consumers are actively seeking alternatives to animal-derived gelatin. Tapioca starch and carrageenan-based softgels allowing non-GMO, vegan, and Halal/Kosher claims are experiencing double-digit growth year-over-year.
- Bioavailability Enhancement via Self-Emulsifying Drug Delivery Systems (SEDDS): Advanced OEM formulations now incorporate natural surfactant lipid carriers that form fine oil-in-water microemulsions upon contact with gastrointestinal fluids, dramatically increasing the absorption rate of lipophilic actives.
- Marketplace Compliance & Amazon Seller Central Readiness: Major platforms enforce stringent documentation rules. Houston suppliers require pre-validated Certificate of Analysis (COA) templates, ISO 17025 accredited third-party lab testing, and verified cGMP accreditation to prevent inventory suppression.
- Customized Color Palette & Brand Differentiation: Standing out on retail shelves requires visual distinction. Modern softgel manufacturing utilizes natural colors (such as chlorophyll, annatto, riboflavin, and purple carrot juice) alongside precise laser branding to deter counterfeiting and enhance brand recognition.
Frequently Asked Questions for Houston & Regional Softgel Buyers
Get clear, authoritative answers regarding minimum order quantities, climate stability, regulatory filings, and custom manufacturing lead times.
How do you address the high humidity of the Houston climate during softgel manufacturing & transit?
Softgels are highly sensitive to moisture. Our manufacturing facility utilizes dehumidified drying chambers maintained under strict RH limits (<20% relative humidity). For storage and transit across the humid Gulf Coast region, products are sealed in high-barrier HDPE bottles with induction foil seals and desiccants, or packed in thermoformed aluminum blister strips to prevent shell softening and clumping.
What are your typical Minimum Order Quantities (MOQs) for custom softgel manufacturing?
For standard private label stock softgel formulations, our minimum order quantity typically starts at 5,000 to 10,000 units (bottles). For fully custom OEM formulations requiring specialized die shapes, custom shell colors, or proprietary active oil fills, production runs generally start at 300,000 to 500,000 bulk softgels, with tiered volume pricing available at 1M+ units.
Can you manufacture non-gelatin vegan softgels for clean-label brands?
Yes. We operate specialized continuous encapsulation lines designed for plant-based softgel production utilizing modified tapioca starch or carrageenan matrices. These shells exhibit excellent thermal stability, high clarity, and are 100% free of animal derivatives, fulfilling Non-GMO, Vegan, Halal, and Kosher certification requirements.
What certifications and compliance documentation do you provide with bulk shipments?
Every production batch is accompanied by a full compliance documentation dossier. This includes a comprehensive finished product Certificate of Analysis (COA) detailing active ingredient potency, heavy metal limits (Lead, Arsenic, Cadmium, Mercury), microbiological purity, gel disintegration time, executed batch record summaries, NSF GMP certificates, and FDA facility registration proof.
What is the standard lead time from initial formula sign-off to final delivery in Houston?
Turnkey custom softgel production generally takes 6 to 8 weeks following artwork and master formula specification sign-off. This timeline includes raw material sourcing, identity verification, pilot pilot encapsulation, full cGMP production, drying, analytical testing, and final packaging. Re-orders with pre-approved raw materials typically ship within 4 to 5 weeks.
Do you support custom oil suspensions with botanical powders or insoluble active ingredients?
Absolutley. Our automated formulation tanks utilize high-shear homogenizers and thermal agitation systems capable of creating ultra-fine, uniform suspension matrices. We micro-grind insoluble powders (such as botanical extracts, minerals, or amino acids) to optimal mesh sizes to ensure non-settling, homogenous fill mass distribution prior to rotary-die encapsulation.
Launch Your Custom Softgel Product Line with Houston's Trusted OEM Partner
Connect directly with our senior R&D chemists and contract manufacturing specialists. Receive a comprehensive quote, request pilot samples, or schedule a facility tour within 48 hours.