Custom Formulations & OEM Bulk Product Portfolio
Explore our turnkey, scalable contract manufacturing capabilities spanning pure dairy proteins, functional botanicals, ergogenic aids, and specialty premixes.
1. Technical Excellence in Whey Protein Manufacturing & Export
As a globally recognized contract manufacturer and exporter of dairy proteins and sports nutrition powders, our manufacturing operations represent the benchmark of pure ingredient processing, strict quality assurance, and formula innovation. In the competitive landscape of B2B nutraceutical supply chains, sourcing high-quality whey protein requires an intimate understanding of membrane separation chemistry, thermal denaturation dynamics, and international regulatory compliance.
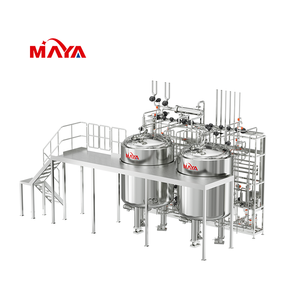
Our facility operates under rigorous NSF GMP, cGMP, and FDA-registered standards, utilizing state-of-the-art Cold Cross-Flow Microfiltration (CFM) technology. Unlike aggressive acid-wash or high-heat extraction protocols that degrade native protein structures, our low-temperature filtration preserves the bioactive fractions essential for immunological health, cellular recovery, and optimal muscle protein synthesis (MPS).
Information Gain Insight: Bioactive whey fractions—such as Immunoglobulins (IgG), Lactoferrin, Bovine Serum Albumin (BSA), and Glycomacropeptides (GMP)—are heat-sensitive. Our non-denaturing filtration maintains over 95% native protein integrity, providing superior biological value (BV = 104) compared to standard commodity dairy powders.
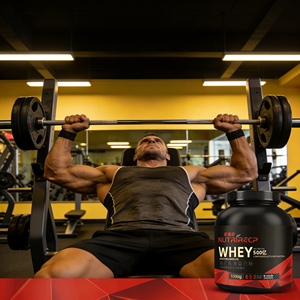
Whey Protein Concentrate (WPC80)
Delivering 80% protein content with natural lipid and mineral matrices for rich mouthfeel, ideal for everyday sports nutrition and meal replacement formulas.
Whey Protein Isolate (WPI90)
Processed through cross-flow ultrafiltration to achieve ≥90% pure protein while eliminating virtually all fat, lactose, and cholesterol for rapid digestion.
Hydrolyzed Whey Protein (WPH)
Enzymatically pre-cleaved into low-molecular-weight di- and tri-peptides for instantaneous GI absorption, hypoallergenic profiles, and peak insulinogenic response.
2. Future B2B Procurement Trends in the Global Whey Market
Procurement directors, supply chain executives, and brand owners must navigate a rapidly evolving global market. Based on proprietary manufacturing data and global export analytics, several macro trends are defining the future of protein powder sourcing over the next decade:
A. Ultra-Clean Labeling & Single-Origin Grass-Fed Verification
Modern consumers actively audit ingredient decks for artificial emulsifiers, synthetic sweeteners, and chemical anti-caking agents. Future-proof procurement requires non-GMO, grass-fed dairy sourcing verified through isotopic testing and certified pasture-raised supply chains. Our manufacturing lines support non-GMO lecithin instantization (utilizing sunflower lecithin over soy lecithin) to fulfill clean-label compliance globally.
B. Targeted Enzyme Fortification for Increased Protein Efficiency
Raw protein intake is shifting toward biological utilization efficiency. Brands are incorporating specialized endo- and exo-peptidase enzyme matrices (such as Prohydrolase®) into whey formulations. These enzymatic systems break down complex protein chains into absorbable amino acids in real-time, reducing GI discomfort, bloating, and nitrogen waste while optimizing plasma Branched-Chain Amino Acid (BCAA) spikes—specifically L-Leucine.
C. Hybrid Formulations: Ergogenic & Nootropic Matrix Integration
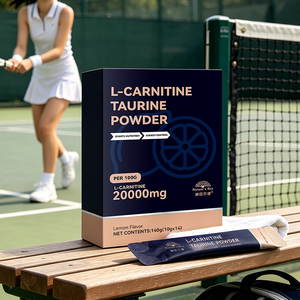
The boundary between classic sports recovery powders and functional wellness beverages has dissolved. Modern contract manufacturing demands homogeneous dry blending of high-purity protein bases with specialized active compounds, including Micronized Creatine Monohydrate, L-Carnitine Tartrate, Electrolyte Osmolality Regulators, and Nootropic Botanicals (e.g., Ashwagandha, Lion's Mane). Our multi-stage batch blenders guarantee an analytical Coefficient of Variation (CV) under 2.5% across all active ingredients.
3. Technological Breakthroughs in Whey Protein Processing
To retain our competitive leadership as a top trusted exporter, our engineering facilities integrate cutting-edge processing advancements that mitigate traditional manufacturing pain points such as clump formation, thermal degradation, and flavor degradation.
Cold-Filtered Native Microfiltration
Directly extracted from raw milk rather than cheese whey bypass, yielding 16% higher L-Leucine concentration and superior structural bioactivity.
Agglomeration & Fluid-Bed Instantization
Custom particle size engineering ensures effortless dispersion in cold liquids within 5 seconds without requiring electric blenders or shakers.
Micro-Encapsulated Flavor Masking
Advanced spray-drying encapsulation neutralizes bitter peptide notes in hydrolyzed proteins while preserving pristine natural flavor notes.
4. Enterprise Manufacturing Strengths & Infrastructure
Our state-of-the-art facility in Fort Myers, Florida spans over 70,000 square feet of cGMP production area, designed specifically to eliminate cross-contamination, guarantee lot-to-lot consistency, and accelerate turnaround times for worldwide distribution.
Unlike standard generic repackers, our contract manufacturing operations feature 17 independent production cleanrooms equipped with positive pressure HVAC systems, HEPA filtration, and strict humidity controls (below 40% RH). This specialized environmental isolation allows us to process sensitive botanical extracts, hygroscopic minerals, probiotics, and pure dairy proteins simultaneously without trace cross-contact.
Turnkey Quality Assurance: Every production lot is paired with a comprehensive Certificate of Analysis (CoA) verified via Third-Party ISO 17025 Accredited Laboratories, validating potency, physical properties, heavy metal compliance, and zero WADA-prohibited substances.
5. Frequently Asked Questions (B2B Procurement FAQ)
Every production run undergoes a rigorous battery of analytical testing prior to release. Raw materials and finished products are tested for Protein Content via AOAC Kjeldahl/Dumas nitrogen analysis, Heavy Metals (Lead, Arsenic, Cadmium, Mercury via ICP-MS), Microbiological Safety (Standard Plate Count, Yeast & Mold, E. coli, Salmonella, S. aureus), Moisture & Ash content, and Allergen verification (gluten and soy cross-contact testing). Certificate of Analysis (CoA) documents accompany every shipment.
For ready-to-brand Private Label stock formulas, our MOQ starts at just 5,000 units. For fully custom formulations involving tailored amino acid decks, specialized flavor development, or custom packaging formats, standard MOQs typically begin at 10,000 units or 1,000 kg of bulk powder. Initial R&D pilot samples are delivered within 5 business days, and turnkey production runs average 8 weeks from final packaging sign-off.
We provide full documentation packages tailored to international import regulations and e-commerce compliance platforms. This includes FDA Facility Registration certificates, NSF cGMP compliance documentation, USDA Organic certifications, Halal and Kosher declarations, Allergen Control Statements, Certificate of Free Sale, and fully audited Supplement Facts panels formatted for US, EU, UK, Middle East, and Latin American market authorities.
Yes. Utilizing cross-flow microfiltered Whey Protein Isolate (WPI90), we can formulate products containing less than 0.5g of lactose per serving, classifying them as lactose-free compliant. Furthermore, our strict environmental cleaning protocols and allergen isolation rooms allow us to certify products as Gluten-Free, Keto-Friendly (low-carb/high-fat), and Soy-Free using sunflower lecithin instantization.
We offer turnkey packaging solutions ranging from retail-ready HDPE/PET tubs, flexible stand-up gusset pouches with resealable zippers, single-serve stick packs, and bulk multi-ply kraft paper bags with polyethylene liners (20 kg / 25 kg) for industrial re-packers. Our export logistics team coordinates palletization, container loading (FCL/LCL), temperature-controlled freight, and export documentation to over 50 countries worldwide.
Partner with a Trusted Global Whey Protein Exporter
Scale your brand with NSF GMP certified quality, high-purity protein formulations, fast sample turnaround, and competitive bulk contract pricing.