Industrial Softgel Manufacturing & Global Supply Chain Catalog
As global nutraceutical consumption pivots toward lipid-based bio-enhanced formulations, selecting a cGMP-certified softgel encapsulation partner is critical. Explore top-tier manufacturing machinery, private-label solutions, and verified softgel capsule dosage lines engineered for maximum active stability.
Medicare Facial Fish Gelatin Softgel Capsule Production Machine with Thickeners & Stabilizers Food Grade
Spot Black Seed Oil Softgels 60 Tablets Adult Improved Bone Density Support O E M Softgel Capsule Making Machine
Automatic Vitamin Gummy Supplement Production Machine for Nutraceutical Softgel Candy Manufacturing Line
OEM Wholesale Custom Softgel Capsule Factory Manufacturer With Gmp/iso/Brc/Halal Adults Bulk Price Oral Liquid Beauty Products
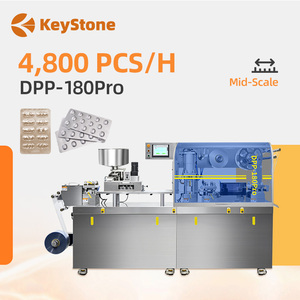
DPP 180pro High Speed 4800 Plates/h Automatic Capsule Packing Machine Tablet Blister Packaging Machine
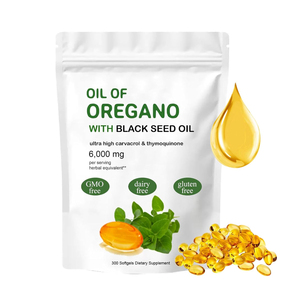
Gmp/iso/halal Manufacturer Private Label Promote Digestion Oregano Oil Carvacrol Softgels Capsules
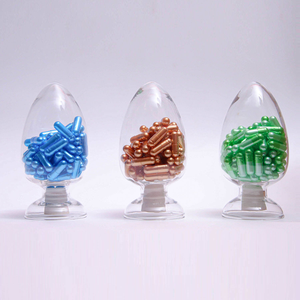
Pharmaceutical Grade Gelatin Empty Capsules 0# 1# 2#3# 4# 300mg 500mg 600mg 1000mg
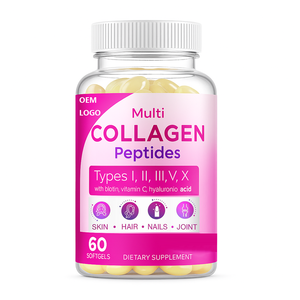
OEM Private Label Collagen Peptides Softgel Capsule Type I II III V X + Biotin Vitamin C Antioxidant 60 Softgels for Adult
The Paradigm Shift in Softgel Encapsulation: Technical Innovations & Future Sourcing Trends
The global soft gelatin capsule market is experiencing unprecedented technological evolutionary leaps. Driven by the convergence of high-potency lipid formulations, hydrophobic botanical extracts, and growing consumer demands for clean-label delivery vehicles, modern contract manufacturers must move beyond basic rotary die encapsulation. Enterprise-level softgel exporters are now evaluated based on their ability to deliver micro-encapsulation stability, control oxygen-permeability coefficients, and master alternative hydrocolloid polymer physics.
To obtain measurable commercial advantages, global distributors and brand owners must align with manufacturers holding pharmaceutical-grade cGMP compliance, robust analytical R&D laboratories, and high-precision rotary die machinery capable of achieving micro-fill precision (±1.5% dosage uniformity). Below is a comprehensive engineering breakdown of the technological parameters defining modern softgel manufacturing excellence.
Hydrocolloid Gel Matrix Engineering
Modern softgel manufacturing leverages bovine, porcine, and fish gelatin matrices combined with precise plasticizers (glycerin, sorbitol, and maltitol). Advanced formulation engineers optimize gel ribbon thickness (0.025 to 0.045 inches) and gel mass viscosity (20,000–30,000 cPoise at 60°C) to prevent shell leaking, cross-linking, and moisture migration in humid export destinations.
Non-Animal Plant & Vegan Shells
The global shift toward plant-based supplements has catalyzed the adoption of modified tapioca starches and carrageenan (seaweed extract) softgel shells. These non-gelatin matrices exhibit superior thermal stability (withstanding storage temperatures up to 40°C/104°F without melting), eliminating clumping during trans-oceanic shipping.
Lipid Bioavailability Enhancement
Softgel encapsulation remains the gold standard for oil-soluble active pharmaceutical ingredients (APIs) and nutraceuticals such as Omega-3 fish oils, Black Seed Oil (Thymoquinone), CoQ10, and Carvacrol Oregano oils. Self-Emulsifying Drug Delivery Systems (SEDDS) are integrated directly into the liquid fill to dramatically enhance human absorption.
Comparative Softgel Shell Matrices & Encapsulation Parameters
Technical evaluation criteria for procurement managers and product development directors.
| Gelatin Shell Type | Primary Raw Ingredients | Thermal Stability Limit | Ideal Active Infill Types | Key Sourcing Advantage |
|---|---|---|---|---|
| Bovine Gelatin (Type A/B) | 100% Pharmaceutical Bovine Hide/Bone | 32°C – 35°C (89.6°F – 95°F) | Lipophilic oils, Vitamin E, Vitamin D3, Omega-3s | Cost-effective, rapid gastric disintegration (< 15 mins) |
| Fish Gelatin (Kosher/Halal) | Deep-sea Fish Scales & Skins | 28°C – 30°C (82.4°F – 86°F) | Beauty-from-within, Collagen Type I/II, Marine Oils | Purity, premium consumer positioning, non-mammalian |
| Tapioca / Vegan Matrix | Modified Tapioca Starch + Carrageenan | 40°C – 45°C (104°F – 113°F) | High-pH fills, Black Seed Oil, Herbal Concentrates | Zero cross-linking, extreme heat resistance, Non-GMO |
| Enteric-Coated Softgel | Gelatin + Methacrylic Acid Copolymer | 35°C (Acid-Resistant in Stomach) | Peppermint Oil, High-Concentrate Carvacrol, Enzymes | Bypasses stomach acid, releases in lower intestine, no burps |
Strategic Softgel Procurement Trends (2025–2030)
1. Micro-Dosing & High-Potency Concentrates
Global buyers are shifting away from large, difficult-to-swallow 1000mg softgels toward highly concentrated micro-softgels (300mg to 500mg). Advanced rotary encapsulation equipment now utilizes precision micro-pumps capable of dosing potent herbal extract lipid solutions with minimal excipient volumes.
2. Nitrogen-Flushed Oxygen Exclusions
Lipid oxidation is the leading cause of rancidity in fish oils and botanical cold-pressed oils. Premier exporters incorporate nitrogen blanketing throughout the entire mixing, holding, and encapsulation stages—ensuring Peroxide Value (PV) and Anisidine Value (AV) levels remain well within strict USP/EP limits.
3. Sustainable Eco-Friendly Packaging Integration
Contract manufacturing must seamlessly transition from traditional HDPE plastic bottles to high-speed blister packaging lines (such as the DPP-180pro system) using recyclable ALU-ALU or cold-form foils. Blister packaging drastically improves individual softgel shelf life by creating hermetic unit-dose moisture barriers.
4. Transparent Supply Chain Compliance & Trackability
Leading international buyers now require complete raw material origin tracing. From Kosher-certified bovine gel sources to non-GMO cold-pressed carrier oils, top factories supply fully trace-back compliant Certificate of Analysis (CoA) records, ISO/BRC/cGMP verification, and heavy metal screening data with every export shipment.
Enova Science & Global Softgel Manufacturing Ecosystem
Operating out of a 70,000 sq. ft. NSF GMP-certified and FDA-registered production complex in Fort Myers, Florida, our manufacturing network provides complete turnkey supplement production. Equipped with 17 independent climate-controlled cleanrooms, full-spectrum R&D laboratories, and high-volume rotary encapsulation lines, we deliver reliable OEM & Private Label export solutions worldwide.
Frequently Asked Questions (FAQ) for Softgel Procurement
Essential technical insights for brand owners, sourcing directors, and pharmaceutical importers.
What are the minimum order quantities (MOQs) for softgel contract manufacturing?
Minimum order quantities for private label stock softgel formulas typically start at 5,000 to 10,000 units. For fully custom formulations requiring specific shell colors, custom shapes (e.g., oval, oblong, twist-off), or proprietary active lipid blends, standard production runs typically start at 100,000 to 300,000 bulk softgels, with tiered volume pricing at higher quantities.
How do you prevent oxidation in sensitive lipid fills like Fish Oil and Black Seed Oil?
We utilize a multi-layered anti-oxidation protocol. All carrier oils are held under a continuous inert nitrogen gas blanket in temperature-controlled stainless steel tanks. During encapsulation, oxygen is excluded from the injection wedge, and finished softgels undergo immediate low-humidity tumble drying followed by sealed tray curing.
What is the difference between gelatin and tapioca/vegan softgels?
Gelatin softgels (bovine, porcine, or fish) utilize collagen proteins that melt around 30°C–35°C and disintegrate rapidly in gastric fluid. Vegan softgels utilize modified food starch (tapioca) blended with carrageenan. Vegan shells withstand higher temperatures (up to 45°C), making them resistant to heat-induced clumping during tropical transport, while fulfilling 100% plant-based label claims.
What lead times can buyers expect for custom softgel manufacturing?
Initial quotation and feasibility reviews are delivered within 48 hours. R&D pilot formulation samples are generated in approximately 5 working days. Once artwork, specifications, and raw materials are finalized, standard turnkey production runs approximately 6 to 8 weeks, including full analytical quality release testing.
What quality assurance testing is provided with softgel export orders?
Every production lot undergoes rigorous cGMP-mandated testing: raw material identity verification via FTIR/HPLC, active ingredient potency assay, disintegration time testing (per USP <701>), microbial limits testing (Total Aerobic Microbial Count, Yeast & Mold, E. coli, Salmonella), heavy metal screening (Lead, Arsenic, Cadmium, Mercury via ICP-MS), and shell seam integrity inspection. A complete Certificate of Analysis (CoA) accompanies every shipment.
Can your facility assist with Amazon compliance and export certificates?
Yes. We supply comprehensive documentation packages tailored to Amazon Seller Central compliance, including GMP Certificates, finished product CoAs, ingredient origin statements, allergen declarations, and Stability Testing documentation. For global exporters, we assist with Certificate of Free Sale (CFS) and export paperwork.
Partner with Top Trusted Softgel Exporters Today
Whether you require high-capacity machinery, bulk gelatin capsules, or ready-to-market private label softgels, our technical team is prepared to analyze your formula brief.