Featured Custom Formulation Products & Systems
Explore our core manufacturing lines, specialized botanical extracts, and automated formulation machinery direct from certified facilities.
The Evolving Architecture of Chinese Supplement Formulation Factories
The global dietary supplement and nutraceutical market has undergone a structural paradigm shift. Sourcing managers and brand operators no longer evaluate contract manufacturers solely on cost per bottle or minimum order quantities (MOQs). Instead, modern supply chain risk management prioritizes analytical integrity, automated batch repeatability, cross-contamination mitigation, and full regulatory traceability. China has emerged as the premier manufacturing powerhouse for complex multi-ingredient formulations, backed by unprecedented industrial automation and refined botanical extraction science.
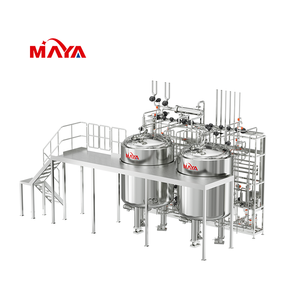
Historically, supplement contract manufacturing relied on semi-automated batching, manual ingredient weighing, and fragmented raw material sourcing. Today, top China supplement formulation factories operate state-of-the-art facilities compliant with international cGMP standards (NSF GMP registered, FDA-registered, ISO 22000, and HACCP certified). By leveraging advanced closed-loop processing machinery—such as the Marya Customized Fully Automated Formulation System—leading manufacturers eliminate human error, guarantee uniform particle distribution, and safeguard thermolabile active compounds.
1. Technical Blueprint of Automated Formulation & Batching Systems
Formulating high-potency nutritional products requires strict control over excipient compatibility, moisture levels, bulk density variations, and shear forces during mixing. In automated production environments, raw material processing undergoes a validated four-stage engineering sequence:
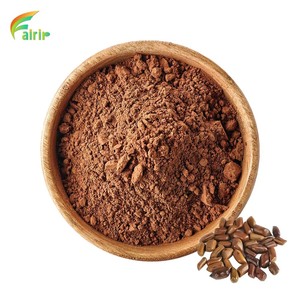
- Micro-Gravimetric Dosing & Liquid Metering: High-precision load cells and automated peristaltic dosing units ensure micronutrients, botanical extracts (like Cassia Seed Extract 10:1), and active lipid matrixes (such as Triple Omega 3-6-9) are weighed to within ±0.05% tolerance.
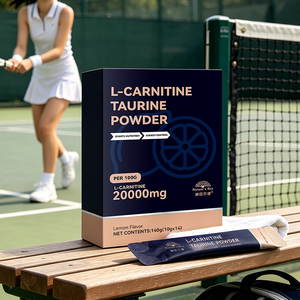
- High-Shear Fluidized Bed Granulation: For sports nutrition powders (e.g., Micronized Creatine Monohydrate and L-Carnitine Taurine Energy matrices), high-shear wet granulation transforms hydrophobic active ingredients into free-flowing, rapidly soluble agglomerates without degrading heat-sensitive vitamins.
- Isolated Cleanroom Batching (ISO Class 7 / Class 8): To comply with stringent international standard guidelines, formulation factories deploy positive-pressure airlocks and dedicated air handling units (AHUs) with HEPA filtration to eliminate airborne particulates and cross-allergen contamination.
- In-Line Process Analytical Technology (PAT): Near-Infrared (NIR) spectroscopy probes continuously monitor blend uniformity in real-time inside 5,000 kg V-blenders, ensuring active pharmaceutical-grade homogeneity prior to encapsulation or sachet filling.
| Formulation Parameter | Legacy Manual Processing | Modern China Automated OEM/ODM Standard | Impact on Finished Product Quality |
|---|---|---|---|
| Dosing Precision | ± 2.0% - 5.0% manual variance | ± 0.05% automated micro-dosing | Guarantees exact label claims without excess ingredient overages. |
| Cross-Contamination Risk | Shared multi-product rooms | 17+ isolated cleanroom suites with CIP | Ensures allergen-free, non-GMO, and strain-pure probiotic batches. |
| Solubility & Flowability | Variable powder particle size | Fluidized-bed spray drying agglomeration | Instantized dissolution for sports powders & electrolyte hydration packs. |
| Heavy Metal Traceability | Batch spot testing | 100% ICP-MS testing per raw material lot | Strict compliance with California Prop 65 & EU heavy metal limits. |
2. Category-Specific Formulation Science & Innovation
China's top formulation factories offer deep expertise across complex delivery systems, catering to diverse wellness segments ranging from clinical cardiovascular support to custom multi-species animal nutrition premixes.
Cardiovascular & Lipid Matrices
Formulating high-yield Triple Omega 3-6-9 Softgels demands strict nitrogen flushing to prevent lipid peroxidation. Factories utilize cold-pressed fish oils and flaxseed extracts, ensuring peroxide values (PV) remain under 3.0 meq/kg for maximum EPA/DHA stability.
Ergogenic & Energy Powders
Synergistic energy solutions blending L-Carnitine, Taurine, and Polydextrose provide sustained athletic stamina without glycemic spikes. Micronized Cassia Seed and Natural Grapefruit flavor systems mask bitter amino acid notes without synthetic additives.
Functional Hydration & Animal Nutrition
Low-carb Electrolyte Hydration Powders utilize chelated trace minerals (Magnesium Bisglycinate, Potassium Citrate) for peak cellular absorption. Similarly, multi-species Animal Feed Mineral Premixes apply micro-encapsulation to protect bio-trace minerals during extrusion pelletization.
Future Sourcing & Procurement Trends in China's Formulation Sector
As brand owners navigate stricter Amazon Seller Central dietary supplement documentation policies, FDA 21 CFR Part 111 audits, and global ESG (Environmental, Social, and Governance) directives, China's contract manufacturing infrastructure is rapidly evolving. Key future trends shaping global supplement sourcing include:
A. Micro-Encapsulation & Liposomal Delivery Vehicles
Standard tablets and capsules face absorption limitations due to stomach acid degradation. Leading China formulation labs are transitioning toward liposomal liquid processing and micro-encapsulated beadlet technology. By shielding sensitive active compounds (such as CoQ10, Creatine, and Probiotics) within phospholipid bilayers, bio-availability is enhanced by up to 500%, unlocking premium brand positioning.
B. Clean-Label Excipient Replacement Science
Global consumers are rejecting synthetic flow agents like Magnesium Stearate, Silicon Dioxide, and Titanium Dioxide. Advanced Chinese OEM factories have engineered organic rice hull concentrates, tapioca maltodextrins, and natural acacia fiber matrices. These organic filler solutions maintain high-speed encapsulation rates while supporting 100% clean-label packaging claims.
C. Full Transparency & Digital Traceability Systems
Modern international buyers require instant verification of raw material origin. Top factories now integrate blockchain-enabled lot tracking. From wild-harvested botanical extraction in rural regions to final blending in ISO cleanrooms, every batch Certificate of Analysis (CoA) is backed by raw analytical data (HPLC, LC-MS/MS, and GC-MS fingerprints).
D. Turnkey Sustainable & Eco-Packaging Integration
Environmental regulations in Europe and North America are driving the adoption of plant-based protein packaging, biodegradable stick packs, and post-consumer recycled (PCR) PET bottles. Sourcing from a facility with integrated zero-waste packaging machinery drastically reduces supply chain carbon footprints and international freight costs.
Why Partner With China’s Leading OEM/ODM Formulation Complexes?
Selecting the right contract manufacturing partner is the single most critical strategic decision for a growing health brand. By combining robust U.S. quality protocols with China's unmatched raw material synthesis and labor efficiencies, certified formulation plants deliver distinct competitive moats:
Full Regulatory Integrity
Facilities hold current NSF cGMP registrations, FDA facility listings, USDA Organic standard validations, Halal sourcing options, and Kosher certification readiness for seamless global customs clearance.
Rapid Pilot Scale R&D
Dedicated R&D laboratories supply custom pilot formulation samples within roughly 5 working days, expediting product validation and reducing time-to-market for private label launches.
Scalable Turnkey Capacity
From 5,000-unit private label runs to high-volume commercial batches of 100,000+ units across gummies, softgels, capsules, stick packs, and powders—our production lines adapt dynamically.
Frequently Asked Questions for Supplement Sourcing & Procurement
Essential technical insights for brand owners, supply chain directors, and retail buyers negotiating custom formulation contracts.
What makes Chinese formulation factories superior for custom OEM/ODM projects?
Top China supplement factories combine direct access to raw ingredient cultivation hubs (such as botanical extract farming regions) with advanced industrial automation like Marya formulation systems. This integration significantly lowers production overhead while enforcing rigid cGMP quality standards, automated batching, and analytical testing comparable to Western pharmaceutical facilities.
How do factories protect sensitive botanical extracts and probiotics during production?
Sensitive botanical actives (like Cassia Seed Extract) and live probiotic cultures are processed in climate-controlled cleanrooms equipped with relative humidity controls (below 30% RH) and low-temperature fluidized-bed micro-encapsulation. Nitrogen blanket flushing is applied during softgel and capsule filling to prevent oxygen-induced active ingredient degradation.
What are the standard Minimum Order Quantities (MOQs) and production lead times?
For ready-to-market private label formulas, MOQs typically start at 5,000 units. Completely custom formulations (such as proprietary Plant-Based Protein or Electrolyte Powder blends) start between 10,000 to 50,000 units depending on dosage form. Technical R&D pilot samples require around 5 working days, while full production turnarounds range between 6 to 8 weeks upon label art sign-off.
What documentation is provided to satisfy Amazon Seller Central & FDA regulations?
Every finished production batch includes a comprehensive compliance dossier: Master Batch Production Records, finished product Certificates of Analysis (CoA) verifying potency, microbiological limits, heavy metal screening (Pb, As, Cd, Hg), stability testing reports, allergen freedom statements, and facility ISO/cGMP certificates required for international sales and Amazon storefront approvals.
Can the factory formulate specialized products like multi-species animal feed mineral premixes?
Yes. Leading contract facilities feature separate dedicated production lines for veterinary and animal nutrition supplements. These lines adhere to specialized feed additive manufacturing guidelines, ensuring accurate trace mineral chelation, anti-caking properties, and homogenous particle sizing across large batch volumes.
Partner with China's Premier Formulation Experts
Transform your innovative supplement concepts into market-ready, regulatory-compliant products. Contact our technical R&D engineering team today for custom formula reviews, pilot samples, and transparent OEM quotations.
Send an Inquiry