Global Private Label & Nutraceutical Contract Manufacturing Excellence
In the rapidly evolving global dietary supplement and functional nutrition landscape, selecting an audited, cGMP-certified contract manufacturer is the single most critical factor for brand security, speed-to-market, and regulatory compliance. Modern brand owners require turnkey partners offering end-to-end capabilities—from precision custom formulation, micro-encapsulation, and stability testing to automated high-speed packaging.
This comprehensive benchmark report evaluates top-tier global private label manufacturers and exporters, establishing technical criteria for operational integrity, ingredient traceability, analytical quality assurance (HPLC/ICP-MS), and supply chain resilience.
High-Demand Private Label Product Formats
Explore ready-to-brand and fully customizable formulation frameworks engineered in NSF GMP-certified facilities. Request technical specs, pilot samples, and bulk tier quotes directly.
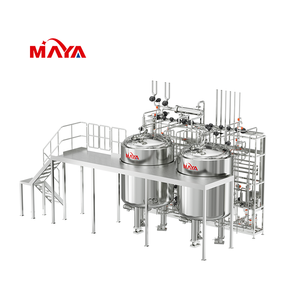
Customized Fully Automated Liquid & Powder Formulation Systems
Turnkey industrial automated mixing, blending, and dosing line integration for high-throughput nutraceutical production.
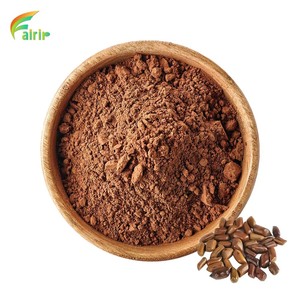
OEM/ODM Custom Formulation Cassia Seed Extract 10:1 Powder
Food-grade standardized botanical extract powder. High purity, cold-water soluble bulk supply for digestive and eye health formulas.
Private Label Micronized Creatine Monohydrate Sports Nutrition Powder
200-mesh ultra-pure micronized creatine monohydrate. Instantized for maximum solubility and rapid ATP regeneration.
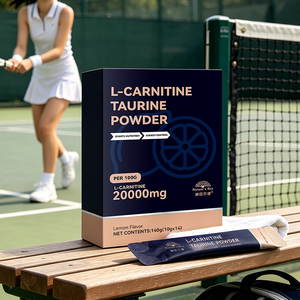
L-Carnitine + Taurine Grapefruit Flavored Energy Supplement Powder
Synergistic metabolic matrix with soluble polydextrose fiber. Custom flavor-masking and zero-sugar sweetener systems.
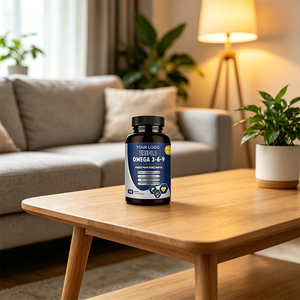
Cardiovascular Support Triple Omega 3-6-9 High-Potency Softgel Capsules
Concentrated EPA & DHA molecularly distilled fish oil blended with flaxseed and borage oils for heart and cognitive longevity.
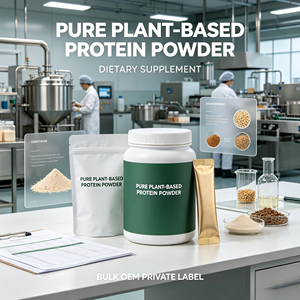
Plant-Based Organic Vegan Protein Powder Dietary Supplement Formulation
Pea, brown rice, and sacha inchi complex providing complete amino acid profile with smooth mouthfeel and zero chalkiness.
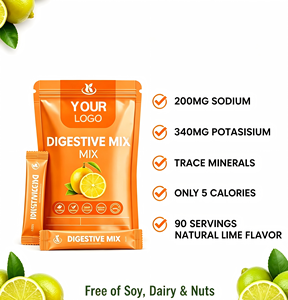
Low-Carb Electrolyte Hydration Powder (Private Label GMP Certified)
Optimal bio-available sodium, potassium, and magnesium ratios for rapid cellular rehydration and endurance performance.
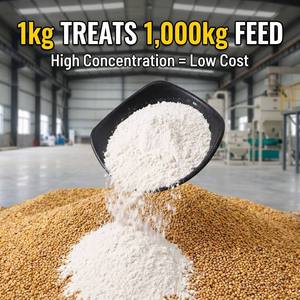
Multi-Species Animal Nutrition Custom Mineral Premix Feed Additive
Micro-encapsulated trace minerals formulated for maximum stability, uniform blending, and superior bioavailability in livestock & pets.
How to Evaluate Top 10 Private Label Manufacturers & Exporters
B2B buyers, sourcing managers, and brand founders must rigorously audit potential OEM/ODM partners. Below is the multi-tier qualification matrix used by enterprise procurement teams when sourcing global contract manufacturers.
1. cGMP & Regulatory Audits
Verify active NSF GMP registration, 21 CFR Part 111 compliance, and FDA facility registration. Full facility audits ensure batch-to-batch consistency and hazard prevention.
2. In-House R&D & Analytical Lab
Top manufacturers maintain internal laboratories equipped with HPLC, ICP-MS, and Fourier-Transform Infrared Spectroscopy (FTIR) for immediate identity, purity, and heavy metal testing.
3. Versatile Dosage Capabilities
Partnership flexibility requires multi-format operations: pectin/gelatin gummies, HPMC two-piece capsules, micro-tablets, liquid droppers, and high-speed powder stick-packs.
4. High-Capacity Speed-to-Market
Ensure scaling potential with facilities operating 5,000+ kg batch blenders, multi-lane rotary encapsulation presses, and automated pouch/bottle packaging machinery.
5. Documentation & Export Files
Seamless international distribution requires full CoA support, allergen matrix documentation, stability study reports, and Amazon Seller Central compliance packets.
6. MOQs & Tiered Pricing
Look for manufacturers offering accessible entry-level stock MOQs (e.g., 5,000 units) alongside competitive economies of scale at 50,000 to 500,000+ unit runs.
Comparing OEM, ODM, and Private Label Manufacturing Models
Understand which manufacturing engagement model aligns with your brand's capital expenditure, timeline, and intellectual property requirements.
| Vector | Private Label Stock Formulas | OEM (Original Equipment Mfg) | ODM (Original Design Mfg) |
|---|---|---|---|
| R&D Lead Time | 1 – 2 Weeks (Pre-Formulated) | 4 – 6 Weeks (Custom Formulation) | 6 – 10 Weeks (Turnkey Concept to Shelf) |
| Formula Ownership | Manufacturer Proprietary | Client Exclusive IP | Co-Developed / Licensed IP |
| Minimum Order Quantity | Low (5,000 Units) | Moderate (10,000 – 25,000 Units) | Higher (25,000+ Units) |
| Flavor & Active Customization | Limited to Stock Flavors | 100% Fully Tailored | Custom Developed by Factory Lab |
| Best Suited For | Fast Market Testing & E-commerce | Established Brands with Active Decks | Innovative Startups seeking R&D Expertise |
Engineering Excellence & Cleanroom Technology
Operating out of a state-of-the-art 70,000 sq. ft. NSF GMP-registered facility in Fort Myers, Florida, our manufacturing operations set the gold standard for global supplement exports.
17 Independent HVAC Cleanrooms
To guarantee zero cross-contamination between potent botanical extracts, active probiotics, and major allergen ingredients, our facility is divided into 17 isolated positive-pressure production rooms equipped with HEPA filtration systems.
Precision High-Speed Encapsulation & Tableting
Utilizing fully automated sub-gram dosage filling lines, we produce hard-shell vegetarian HPMC, gelatin, and pullulan capsules in sizes 000 through 3, alongside dual-layer, chewable, and enteric-coated tablet configurations.
Advanced Micro-Encapsulation & Liquid Filling
Our specialized R&D lab specializes in protective micro-encapsulation for moisture-sensitive probiotic strains and bio-fermented enzymes, extending shelf-life potency without degradation.
Full Analytical & Stability Testing Protocols
Every raw material undergoing intake is quarantined and subjected to FTIR identity verification, microbiological limit assays, heavy metal screening via ICP-MS, and pesticide residue testing prior to release.
Next-Generation Product Development & Global Procurement Trends
As consumer expectations shift toward clean-label transparency and scientific validation, contract manufacturing is undergoing key technological transformations. Brands must align with exporters leveraging these macro trends:
Pectin-Based Sugar-Free Gummies
Traditional gelatin is rapidly being replaced by tapioca-based non-GMO pectin matrices. Active ingredients like creatine, liposomal vitamin C, and elderberry require low-heat depositing to preserve active potency.
Spore-Forming Biotics & Postbiotics
Standard lactobacillus strains suffer heat loss during shelf-life. Formulators are shifting to room-temperature stable spore-forming Bacillus coagulans and heat-treated postbiotic metabolites.
Single-Serve Travel Stick Packs
On-the-go consumer lifestyles are driving demand away from heavy 2lb plastic tubs into lightweight, moisture-barrier laminate stick packs for hydration electrolytes and greens powders.
Accelerate Your Product Launch with USA-Based cGMP Production
Whether you require turn-key private label stock formulas or complex high-potency custom formulations, our R&D chemists and manufacturing specialists are ready to review your project brief within 48 hours.
Frequently Asked Questions by Global Sourcing Managers
Get direct technical insights regarding lead times, regulatory compliance, testing protocols, and custom formulation workflows.
Do you support both custom formulations (OEM) and private label stock products?
What are your minimum order quantities (MOQs) for custom and stock runs?
What are the standard lead times from formula approval to shipment?
What certifications and regulatory standards does your facility maintain?
What analytical testing and quality documentation is supplied with each order?
Can you assist with Amazon Seller Central compliance and export documentation?
5-Stage Turnkey Contract Manufacturing Workflow
Our standardized product lifecycle ensures total transparency, risk mitigation, and strict quality control from raw material intake to global delivery.
Scope & Formulation Brief
Define active ingredient deck, target potency, serving size, flavor profile, dosage format, and packaging expectations with our technical sales engineers.
R&D Pilot & Flavor Optimization
In-house chemists formulate benchtop samples, evaluate excipient flowability, test active stability overages, and refine flavor masking systems for client approval.
Raw Material Intake & QC
Quarantine incoming raw ingredients, perform FTIR identity validation, assay pure actives, and conduct heavy metal/microbial clearance prior to release for production.
cGMP High-Speed Production
Execute batch blending, precision encapsulation/tableting/depositing, in-line checkweighing, and automated bottling or stick-pack pouching inside positive-pressure cleanrooms.
Analytical Release & Export
Final product analytical testing, Quality Assurance sign-off, CoA generation, palletization, and white-glove export logistics handling to your global distribution hubs.
Ready to Scale Your Supplement Line with a Trusted Manufacturer?
Download our complete OEM/ODM product catalog, request custom formula quotations, or schedule a facility tour of our NSF GMP-registered plant in Fort Myers, Florida.