Turnkey OEM/ODM Softgel & Custom Formulation Solutions
Explore our high-performance dietary supplement products and fully customizable encapsulation options engineered for optimal bioavailability, superior shell integrity, and international regulatory compliance.
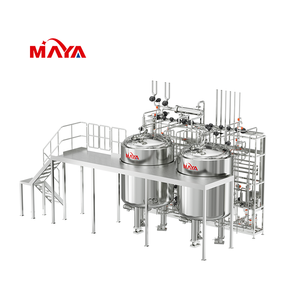
Fully Automated Softgel Formulation & Liquid Dosing System
Precision-engineered automated liquid formulation equipment ensuring seamless thermal jacketed mixing, de-aeration, and tight fill-weight tolerances for complex lipophilic matrices.
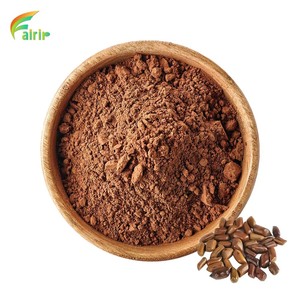
OEM/ODM Cassia Seed Extract 10:1 Botanical Softgel & Powder
High-purity botanical extract standardized 10:1 ratio. Formulated for ocular wellness and metabolic digestive balance, available in oil suspension softgels or botanical powders.
Custom Sports Nutrition Creatine Monohydrate & Bio-Softgel Solutions
Ultra-micronized creatine monohydrate engineered for enhanced solubility and cell hydration. Available in bulk formulation, custom powders, and suspension softgel formats.
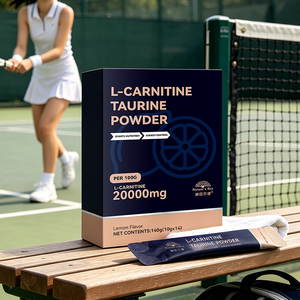
Private Label L-Carnitine + Taurine Energy Softgel & Powder Complex
Synergistic metabolic matrix accelerating fatty acid transport and cellular stamina. Customized with natural grapefruit flavor notes and optimal moisture-barrier encapsulation.
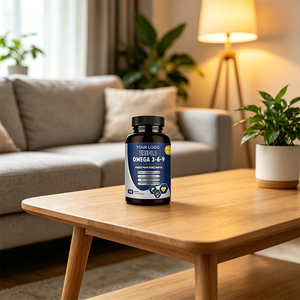
Cardiovascular Health Triple Omega 3-6-9 EPA/DHA Softgel Capsules
Premium molecularly distilled deep-sea fish oil combined with flaxseed and borage oils. Standardized EPA/DHA ratios designed to support cardiovascular and cognitive function.
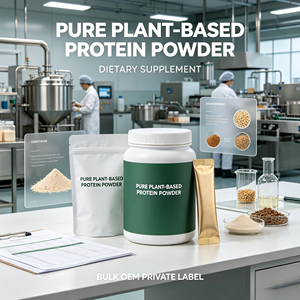
Plant-Based Protein & Vegan Softgel Custom OEM Formulation
100% clean-label plant-based protein blends and non-GMO tapioca softgel shells. Zero gelatin, allergen-free, and ideal for modern vegan supplement brand positioning.
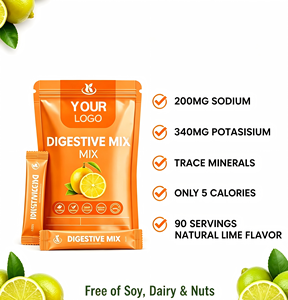
Custom Low-Carb Electrolyte & Heart Healthy Hydration Softgel/Powder
Rapid-absorption ionic mineral formulation supporting cellular electrolyte balance, endurance, and cardiovascular health. Produced in our cGMP certified U.S. facility.
Custom Trace Mineral Premix & Bio-Active Oil Softgel Formulation
Micro-encapsulated chelated trace minerals engineered to prevent oxidation in lipid suspensions. Optimized for multi-species animal nutrition and human health supplements.
Why Leading Global Brands Partner With Our Facility
From initial R&D pilot batches to full-scale automated softgel rotary die encapsulation, we deliver complete contract manufacturing transparency and clinical-grade quality assurance.
NSF GMP & FDA Registered Infrastructure
Our state-of-the-art facility operating in Fort Myers, Florida adheres strictly to 21 CFR Part 111 cGMP standards. Every batch is manufactured under positive pressure HEPA-filtered cleanroom suites to guarantee zero cross-contamination.
Advanced Rotary Die Encapsulation
Utilizing ultra-precise water-cooled rotary die encapsulation machinery, we deliver strict fill-weight consistency (+/- 1%), optimal ribbon thickness control, and hermetically sealed seams for extended shelf life.
Comprehensive Analytical Quality Control
In-house testing laboratories equipped with HPLC, GC-MS, and ICP-MS systems execute rigorous raw material identification, active ingredient potency verification, heavy metal screening, and microbial limits analysis.
Technical Excellence in Softgel Encapsulation: Chemistry, Bioavailability, and Delivery Mechanics
Softgel encapsulation represents one of the most sophisticated oral delivery systems in modern nutraceutical and pharmaceutical contract manufacturing. Unlike conventional compressed tablets or hard gelatin capsules, soft gelatin and plant-based softgel capsules are liquid-sealed single-piece structures designed to protect sensitive lipophilic actives, enhance gastrointestinal absorption, and eliminate unpleasant odor or taste profiles.
1. Gelatin Matrix vs. Plant-Based Tapioca/Pectin Encapsulation
Selecting the correct shell matrix is critical to ensuring chemical stability and preventing shell-to-fill interactions during shelf storage:
- Bovine & Porcine Gelatin Shells: Standard gelatin softgels utilize high-Bloom pharmaceutical gelatin (typically 150–200 Bloom) plasticized with glycerin or sorbitol. Gelatin offers high tensile strength, excellent elasticity during high-speed rotary die encapsulation, and rapid gastric disintegration (under 15 minutes).
- Vegetarian Tapioca & Carrageenan Shells: To satisfy global vegan, Halal, and Kosher consumer demand, advanced non-animal softgel technology utilizes modified tapioca starch combined with seaweed-derived carrageenan and pectin. These vegan softgel shells provide superior thermal resistance (up to 45°C), lower moisture permeability, and zero risk of cross-linking when encapsulating aldehyde-rich botanical extracts.
2. Overcoming Softgel Cross-Linking & Oxidation
Gelatin cross-linking occurs when reactive aldehydes, trace heavy metals, or high humidity induce covalent bonding between gelatin protein chains, creating an insoluble pellicle that retards dissolution. As a master contract manufacturer, our facility mitigates cross-linking via four engineered protocols:
Nitrogen Blanket Protection
Fill preparation and encapsulation hoppers are constantly flushed with food-grade nitrogen gas to displace dissolved oxygen, preventing Peroxide Value (PV) spikes in sensitive Omega oils.
Precision Equilibrium Humidity Control
Multi-stage continuous drying tunnels maintain strict 18–22% Relative Humidity (RH) and 20°C temperatures, achieving precise shell moisture content (6–8%) without thermal stress.
Future Procurement Trends in Softgel Manufacturing
B2B buyers, private label brands, and pharmaceutical distributors must navigate evolving consumer preferences, clean-label regulations, and supply chain dynamics over the next decade.
1. Exponential Shift Toward Plant-Based Vegan Softgels
Global B2B demand for non-animal softgels is projected to grow at a CAGR of 8.4% through 2030. Brand procurement teams are phasing out animal gelatin in favor of Non-GMO tapioca starch and carrageenan shells to tap into plant-based, Halal, Kosher, and environmentally conscious demographics.
2. High-Potency Liposomal & Suspension Softgels
Modern consumers demand smaller softgel sizes with higher active concentration. Procurement is transitioning from simple oil solutions to complex Self-Emulsifying Drug Delivery Systems (SEDDS), liposomal lipid carriers, and micro-suspensions that increase cellular uptake by up to 500%.
3. Supply Chain Traceability & ESG Compliance
Regulatory bodies including the US FDA, EFSA, and Amazon Seller Central require absolute transparency regarding raw material origins. B2B buyers now prioritize manufacturers offering full lot traceability, MSC-certified marine oils, and sustainable botanical sourcing.
4. Targeted Intestinal Delivery & Enteric Softgels
Standard softgels release contents in the acidic stomach environment. The future of targeted gut-health, enzyme, and probiotic softgels relies on intrinsic enteric softgel shell technology that bypasses stomach acid to disintegrate specifically in the alkaline small intestine without synthetic chemical coatings.
5. Clean-Label Excipient Elimination
Synthetic plasticizers, artificial colors (such as Titanium Dioxide), and GMO carrier oils are being rapidly eliminated from brand formulations. Procurement trends emphasize naturally colored softgel shells utilizing chlorophyll, caramel, and fruit extracts with organic virgin olive or coconut oil carriers.
Industry Development Trends & Technological Breakthroughs
The global softgel encapsulation market is rapidly advancing toward high-precision micro-dosing, multi-phase liquid delivery, and automated computer-vision quality inspection.
Dual-Chamber & Beadlet-in-Softgel Technology
Combining incompatible ingredients inside a single dosage unit is now possible. Advanced rotary die systems can encapsulate solid micro-beadlets or secondary micro-capsules suspended within an outer liquid oil matrix, delivering delayed-release multi-stage bioavailability.
Cold-Press & Odor Encapsulation Engineering
Temperature-sensitive active ingredients like live probiotics, omega oils, and fragile enzymes degrade under conventional hot-gelatin casting. Emerging cold-seal and ultra-low temperature casting techniques preserve 99%+ active potency while completely locking in unpleasant odors.
B2B Softgel Encapsulation Procurement FAQ
Detailed answers to critical technical, regulatory, minimum order quantity (MOQ), and manufacturing lead-time questions for supplement brand owners and buyers.
What are your Minimum Order Quantities (MOQs) for custom softgel manufacturing?
Our standard minimum order quantity for ready-to-brand private label stock softgel formulas starts at 5,000 bottles (or bulk equivalent). For fully custom softgel formulations requiring custom shell tooling, specialized active suspensions, or non-standard dies, custom runs typically start at 300,000 bulk softgels, with tiered volume pricing discounts at 500,000, 1,000,000, and 3,000,000+ units.
What is the standard turn-around time from formula approval to finished product release?
Initial quote generation occurs within 48 business hours. R&D pilot sample creation takes approximately 5–7 business days. Upon final customer sign-off on master specifications, artwork proofs, and pilot samples, turnkey production runs typically take 6 to 8 weeks, depending on raw material sourcing and packaging component lead times.
Do you produce both bovine gelatin and vegetarian plant-based softgels?
Yes. Our Fort Myers, Florida facility operates dedicated production lines for traditional bovine/porcine gelatin softgels as well as 100% plant-based tapioca starch and carrageenan vegan softgels. Both formats can be customized with organic certified carrier oils, natural colorants, and specialized shapes (oval, oblong, round, chewable, or twist-off).
What documentation do you provide for Amazon Seller Central and global export compliance?
Every production batch is accompanied by a full cGMP documentation package, including an official Certificate of Analysis (CoA) from an ISO 17025 accredited laboratory, Finished Product Specifications, Master Batch Records summary, Allergen Statements, Stability Data, and NSF/FDA compliance certificates required by Amazon Seller Central, US Customs, and international health authorities (EFSA, TGA).
How do you prevent softgels from leaking, sticking, or degrading during transit?
We control softgel seal integrity through automated optical laser inspection system checks during rotary die encapsulation. Furthermore, post-encapsulation tumble drying achieves precise equilibrium Relative Humidity (eRH), and finished bottles include food-grade silica desiccant packs, induction heat-sealed neck seals, and climate-controlled storage to guarantee shell stability during transit.
Can your laboratory help formulate complex active suspensions or oil blends?
Absolutely. Our senior formulation R&D team specializes in solubilizing difficult hydrophobic powders (e.g., CoQ10, Resveratrol, Curcumin, Botanical Extracts) into bioavailable oil suspensions using lecithin, medium-chain triglycerides (MCT oil), or proprietary self-emulsifying vehicle blends.
Ready to Build Your Custom Softgel Product Line?
Partner with an NSF-GMP certified, FDA-registered U.S. contract manufacturer. Get expert R&D guidance, precise rotary die encapsulation, and competitive factory-direct volume pricing.