Precision Engineered Formulation Formats
Explore our flagship OEM/ODM custom formulations, engineered for maximum bio-accessibility, verified label accuracy, and rapid market deployment.
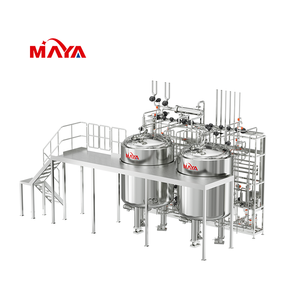
Custom Fully Automated Formulation System
State-of-the-art closed-loop automated formulation and processing architecture designed for ultra-precise liquid, powder, and emulsion dosing under cleanroom conditions.
Get a Quote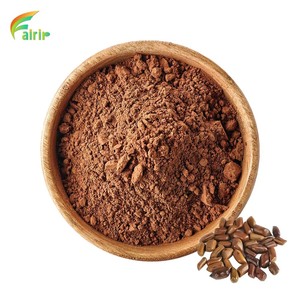
Cassia Seed Extract 10:1 Food Grade Powder
Standardized 10:1 botanical extract featuring high anthraquinone potency. Solvent-free water extraction tailored for digestive health and metabolic formulas.
Get a Quote
Ultra-Micronized Creatine Monohydrate Powder
200-mesh micronized athletic performance powder engineered for instantaneous liquid dispersion, optimal cellular hydration, and ATP regeneration matrix support.
Get a Quote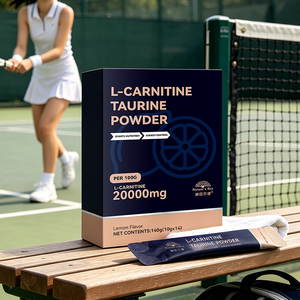
L-Carnitine Taurine Energy Powder Drink Mix
Synergistic metabolic matrix combining free-form L-Carnitine, Taurine, and Polydextrose fiber with custom grapefruit flavor optimization for sustained physical stamina.
Get a Quote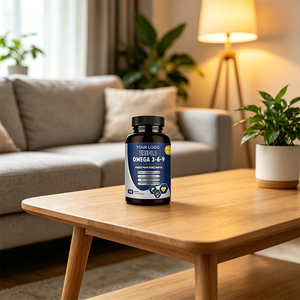
Cardiovascular Health Triple Omega 369 Softgels
Pharmaceutical-grade cold-pressed marine and botanical lipid complex delivering standardized EPA, DHA, ALA, and GLA ratios for cellular lipid membrane integrity.
Get a Quote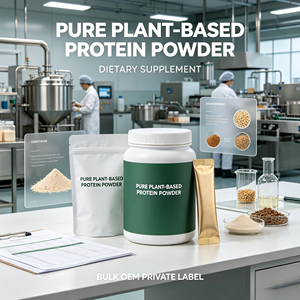
Organic Plant-Based Vegan Protein Powder
Complete amino acid profile synthesized from organic yellow pea, brown rice, and sacha inchi. Smooth texture profile with zero gritty sedimentation or bitter off-notes.
Get a Quote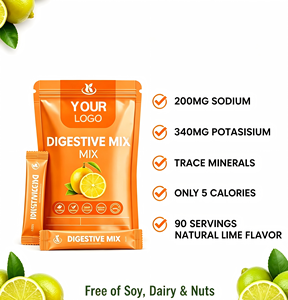
Low-Carb Rapid Hydration Electrolyte Powder
Osmolality-optimized ionic mineral electrolyte system containing bioavailable Potassium Citrate, Magnesium Malate, and Sodium Chloride for cellular rehydration.
Get a Quote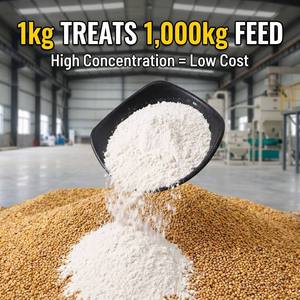
Multi-Species Mineral Premix Feed Additive
High-stability micro-mineral matrix (Zinc, Manganese, Copper, Selenium) formulated for animal nutritional fortification, superior shelf retention, and bio-absorption.
Get a QuoteThe Paradigm Shift in Contract Nutraceutical Manufacturing
An executive report on bio-accessibility engineering, regulatory compliance shifts, clean-label transparency, and global supply chain optimization for 2025–2030.
1. Clean-Label & Synthetic Excipient Elimination
Modern consumers actively scrutinize ingredient decks. Contract manufacturing is rapidly moving away from synthetic binders like magnesium stearate, silicon dioxide, and artificial colors. Our facility utilizes natural organic rice hull matrices, tapioca dextrins, and botanical flow agents to deliver clean-label integrity without compromising high-speed tableting or encapsulation throughput.
2. Precision Bio-Availability Engineering
It is no longer enough to offer unformulated raw actives. Advanced OEM/ODM projects incorporate micronization, liposomal encapsulation, and self-emulsifying drug delivery systems (SEDDS). These technological enhancements significantly improve mucosal absorption rates, overcome first-pass liver metabolism, and provide measurable kinetic advantages for fat-soluble vitamins, botanicals, and lipophilic active compounds.
3. Stringent Global Regulatory Oversight
Cross-border supply chains require absolute regulatory synchronization. From FDA 21 CFR Part 111 cGMP compliance in North America to EFSA regulatory standards in Europe and Amazon Seller Central compliance verification, contract manufacturers must provide complete end-to-end analytical traceability, lot lineage, and verified stability documentation.
Inside Our 70,000 Sq. Ft. cGMP Manufacturing Facility
Combining automated material processing, segregated environmental cleanrooms, and high-throughput blending architectures to deliver flawless batch-to-batch consistency.
Advanced Dosage Form Capabilities
Our plant operates specialized automated lines for a vast array of consumer delivery formats, ensuring maximum stability, physical durability, and precise organoleptic profiles:
- Two-Piece Capsules: Hard gelatin, HPMC (vegetarian), and pullulan capsules in sizes 000 to 4, including delayed-release acid-resistant enteric formulations.
- Precision Compressed Tablets: Monolayer, bi-layer, chewable, sublingual, and effervescent tablets with custom tooling, debossing, and moisture-barrier film coatings.
- Nutraceutical Gummies: Pectin and gelatin bases, sugar-free polyol matrices, custom mold geometries, and heat-stable active ingredient deposition systems.
- Powder Blends & Stick Packs: Bulk powders, single-serve moisture-barrier sachets, and stick packs for hydration, greens, and protein formulas with rapid mixability.
- Nutraceutical Liquids & Tinctures: Aqueous solutions, oil-based drops, sublingual sprays, and functional beverages with validated shelf-life antimicrobial preservation systems.
Rigorous Cross-Contamination Control Protocols
Cross-contamination is the primary vulnerability in high-volume contract manufacturing. Our facility utilizes a strict containment infrastructure to protect brand integrity:
- 17 Independent Cleanrooms: Dedicated environmental controls utilizing positive-to-negative air pressure cascades to isolate potent actives, botanicals, and allergens.
- HEPA Filtration Systems: Continuous HVAC air turnover with 99.97% particulate filtration down to 0.3 microns, controlling ambient humidity ($<40\% RH$) for moisture-sensitive hygroscopic ingredients.
- Validated CIP (Clean-in-Place) Protocols: Swab testing and ATP bioluminescence validation between production runs to ensure complete removal of residual proteins and actives.
- Dedicated Allergen Isolation: Dedicated equipment trains for soy, dairy, nut, and gluten processing to prevent cross-contact risks.
Analytical Testing & Verification Protocol Comparison
A detailed view of how our laboratory protocol elevates brand security compared to standard industry baseline practices.
| Quality Control Stage | Baseline Industry Standard | Enova Science Advanced OEM Standard | Commercial Value to Brand Owner |
|---|---|---|---|
| Raw Material Intake | Basic Supplier Certificate of Analysis (CoA) review with spot testing. | 100% Raw Material FTIR/NIR identity testing, heavy metals (ICP-MS), pesticides (LC-MS/MS), and bio-burden screening prior to release from quarantine. | Eliminates adulterated or out-of-spec raw ingredients before formulation begins. |
| In-Process Blending | Visual inspection & basic weight check. | High-Performance Liquid Chromatography (HPLC) assay of blend samples taken from multiple mixer points to verify homogenous active distribution. | Prevents hot-spotting of high-potency ingredients and guarantees label claim accuracy. |
| Stability Verification | Estimated shelf-life based on raw ingredient data sheets. | Real-time and accelerated shelf-life testing ($40^\circ\text{C} / 75\% \text{RH}$) per ICH guidelines with active potency decay profiling. | Defends brand against premature decay, consumer returns, and regulatory recalls. |
| Marketplace Compliance | Standard batch record delivery on request. | Turnkey documentation packages tailored for Amazon Seller Central, US FDA audit trail readiness, Health Canada, and EU regulatory filings. | Accelerates product listing approvals and international market entry. |
The 6-Stage OEM/ODM Contract Manufacturing Roadmap
From initial formula architecture to global container shipment, our standardized workflow guarantees speed-to-market without compromising scientific rigor.
Formula Consultation & Scope
We review your target ingredient deck, dosage delivery goals, target price per unit, and desired regulatory claims. Our R&D chemists evaluate active compatibility, particle morphology, and stability feasibility.
R&D Prototyping & Sampling
Our in-house R&D laboratory formulates pilot samples within 5 business days. We optimize organoleptic flavor profiles, color aesthetics, flowability, and dissolution rates for your final approval.
Regulatory Review & Specifications
We finalize Master Manufacturing Records (MMR), approve raw material spec sheets, verify label compliance against FDA 21 CFR Part 101 guidelines, and lock in turn-key packaging component artwork.
cGMP Commercial Batch Execution
Raw materials are released from quarantine following 100% analytical testing. Blending, high-speed encapsulation/tableting, and primary packaging proceed in segregated cleanrooms under strict Batch Production Records (BPR).
Finished Product Analytical Testing
Finished goods undergo final laboratory testing for active potency assay, microbiological limits (E. coli, Salmonella, Yeast & Mold), and heavy metals (Lead, Arsenic, Cadmium, Mercury).
Quality Release & Global Logistics
Upon final review by Quality Assurance, a comprehensive Certificate of Analysis (CoA) is issued. Goods are released for palletized distribution, fulfillment center routing, or global export.
Frequently Asked Procurement & Technical Questions
Expert guidance addressing minimum order volumes, IP ownership, scaling, custom formulation, and compliance standards.
What distinguishes fully custom OEM formulations from standard private label stock formulas?
Custom OEM (Original Equipment Manufacturer) formulation involves creating a unique, proprietary ingredient deck tailored precisely to your brand's specific functional goals, active dosage requirements, flavor profiles, and target market claims. You maintain intellectual ownership over the bespoke formula. Private Label ODM (Original Design Manufacturer) solutions utilize pre-developed, stability-tested stock formulations where you apply your custom branding and packaging, enabling rapid market launching with minimal initial R&D expenditure.
What are your Minimum Order Quantities (MOQs) across different dosage formats?
Our facility accommodates both emerging scale-up brands and established enterprise corporations. Private label stock formulas typically start at 5,000 bottles or units. Fully custom OEM formulations vary by form factor: custom encapsulated products generally start at 10,000 bottles (or 300,000 capsules); custom tablets start at 10,000 units; custom powder blends start at 1,000 kg total blend volume; and specialized gummy or stick-pack lines require minimum runs based on raw active costs and packaging geometry. Tiered volume discounts apply at 25,000, 50,000, and 100,000+ unit thresholds.
What standard turn-around times (lead times) can we expect for repeat production orders?
Initial turnkey custom projects typically require 6 to 8 weeks following final artwork sign-off, pilot sample approval, and raw material procurement verification. Repeat production orders benefit from pre-qualified raw material pipelines and established Batch Master Records, reducing turn-around time to approximately 4 to 6 weeks depending on packaging complexity and secondary lab testing timelines.
How does your facility manage delicate or hygroscopic active ingredients?
We operate specialized environmental cleanrooms with dedicated dehumidification systems capable of maintaining relative humidity below 30% RH and controlled ambient temperatures. For sensitive probiotic strains, enzymes, and botanical extracts prone to moisture degradation or heat thermal decay, we utilize microencapsulated raw materials, nitrogen-flushed primary packaging, and low-temperature batch blending techniques to preserve bio-activity throughout shelf life.
What documentation do you provide for international market export and retail listing?
Every manufactured batch is delivered with a complete compliance package. This includes executed Master Batch Record summaries, finished product Certificates of Analysis (CoA) from accredited laboratories, Allergen Statements, GMO Declarations, Stability Testing Summaries, Certificate of Free Sale (CFS), and cGMP Facility Certification. These documents support smooth listing approvals across Amazon Seller Central, major brick-and-mortar retail networks, and international customs entry points.
Who retains the Intellectual Property (IP) rights for custom-developed formulas?
When you partner with Enova Science for a custom OEM formulation project under a formal Development Agreement, your brand retains full ownership of the final commercialized formula deck, active ratios, and custom flavor profiles upon completion of contractual obligations.
Ready to Commercialize Your Next Custom Formulation?
Speak directly with our senior formulation scientists and contract manufacturing directors. Receive detailed feasibility analysis, formula review, and transparent wholesale quotations within 48 hours.
Get a Quote