High-Demand Bulk Formulations & Contract Manufacturing
Explore our export-ready bulk capsules, botanical extracts, sports nutrition powders, and automated compounding capabilities.
World-Class Contract Manufacturing Engineering for Global Brands
As global dietary supplement brand owners, pharmaceutical distributors, and retail importers navigate an increasingly complex regulatory landscape, securing a reliable, highly scalable, and fully compliant Custom OEM Bulk Capsules Factory & Exporter is paramount. Operating out of a state-of-the-art 70,000 square foot NSF cGMP-registered and FDA-inspected facility in Fort Myers, Florida, our enterprise delivers end-to-end contract manufacturing, custom powder blending, automated capsule filling, micro-encapsulation, and export documentation services to over 50 countries worldwide.
Modern capsule contract manufacturing goes far beyond simple powder filling. It demands rigorous raw material physical characterization, exact particle size distribution (mesh sizing), moisture migration control, excipient compatibility evaluation, and strict adherence to U.S. FDA 21 CFR Part 111 standards. Our facility utilizes 17 independent, positive-pressure cleanroom suites equipped with high-efficiency particulate air (HEPA) filtration systems to prevent cross-contamination, ensuring that sensitive botanical extracts, hygroscopic minerals, delicate probiotics, and high-potency sports nutrition actives maintain their absolute purity and target potency throughout the production lifecycle.
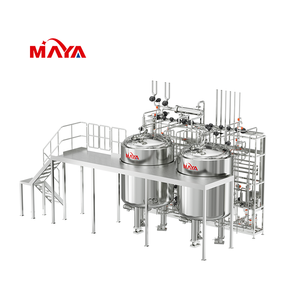
Automated Compounding Systems
Fully automated ingredient dosing and high-shear V-blenders (up to 5,000 kg capacity) ensure homogeneous mixing for multi-ingredient complex formulations without thermal degradation of active compounds.
Multi-Shell Material Options
We process standard Bovine/Porcine Gelatin, Non-GMO HPMC (Hydroxypropyl Methylcellulose) Vegetable Shells, Clean-Label Pullulan, and Enteric-Coated Acid-Resistant Shells from Size 000 to Size 4.
Global Market Compliance
Every bulk shipment includes complete documentation: Certificates of Analysis (CoA), Heavy Metal testing, Microbe counts, Stability data, USDA Organic support, Halal & Kosher certificates, and Amazon CoA compliance.
Advanced Capsule Science: Formulations, Disintegration & Bioavailability
The efficacy of a dietary supplement capsule depends fundamentally on its disintegration profile, dissolution kinetics, and bioavailability within the human gastrointestinal tract. As a leader among international OEM capsule exporters, our dedicated R&D lab engineers tailored encapsulation solutions based on the specific bio-chemical characteristics of your active deck.
1. Gelatin vs. HPMC vs. Pullulan Hard Shell Technology
Selecting the optimal capsule shell material is a crucial first step in custom supplement formulation:
- Hard Gelatin Capsules (HGC): Derived from high-grade collagen, gelatin shells offer superior oxygen-barrier properties, low cost, and fast gastric disintegration (typically under 15 minutes per USP <2040> standards). Ideal for non-hygroscopic dry powders.
- HPMC Vegetable Capsules: Hydroxypropyl Methylcellulose (HPMC) capsules contain low moisture content (4%–6% compared to gelatin’s 13%–16%), making them the premier choice for hygroscopic botanical extracts, moisture-sensitive vitamins, and strict vegan/vegetarian product positioning.
- Pullulan Natural Capsules: Produced via natural tapioca fermentation, Pullulan offers an impermeable barrier to oxygen, protecting sensitive actives like resveratrol, CoQ10, and lipids against oxidative degradation without synthetic chemical modifications.
- Acid-Resistant Delayed-Release Capsules: Designed to pass through the acidic stomach environment intact and release active ingredients in the upper intestine. Essential for digestive enzymes, SAM-e, and probiotic strains.
| Capsule Type | Moisture Content | Oxygen Permeability | Primary Target Actives | Target Disintegration Time |
|---|---|---|---|---|
| Standard Gelatin | 13.0% – 16.0% | Low | Amino acids, minerals, non-hygroscopic powders | < 15 minutes (Gastric) |
| HPMC Vegetable | 4.0% – 7.0% | Moderate | Botanical extracts, herbal powders, hygroscopic vitamins | < 20 minutes (Gastric) |
| Pullulan Tapioca | 10.0% – 14.0% | Extremely Low | Antioxidants, oxygen-sensitive herbal complexes | < 15 minutes (Gastric) |
| Acid-Resistant HPMC | 4.0% – 6.0% | Moderate | Probiotics, enzymes, targeted intestinal release formulations | Dual-stage (>60 min Stomach / <30 min Intestine) |
2. Particle Size Reduction & Granulation Dynamics
A frequent challenge in bulk capsule manufacturing is powder separation or poor flowability during high-speed encapsulation. To achieve fill-weight uniformities within strict USP thresholds (CV < 2%), our factory utilizes fluid-bed granulation, roller compaction (dry granulation), and micro-milling. By homogenizing particle sizes between 60 mesh and 200 mesh, we eliminate void spaces and static charges within the encapsulation machine’s dosing disk, guaranteeing consistent active dosing across millions of capsules.
3. Micro-Encapsulation and Liquid-Filled Hard Capsules (LFHC)
For lipid-based ingredients, fat-soluble vitamins (Vitamin D3, K2, E), and botanical oils (such as Saw Palmetto or Black Cumin Seed Oil), our OEM plant provides Liquid-Filled Hard Capsule (LFHC) technology. Utilizing dual-ring hermetic band sealing, we prevent oil leakage, mask unpleasant organoleptic notes, and significantly boost bioavailability compared to conventional powder blends.
Analytical Precision & Batch Quality Assurance
Our Fort Myers laboratory adheres to rigorous analytical testing protocols for every production batch. Raw materials are quarantined and verified via FT-IR Spectroscopy and High-Performance Liquid Chromatography (HPLC) for identity and assay potency. Finished bulk capsule lots undergo Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metal analysis (Lead, Cadmium, Arsenic, Mercury) and USP <61/62> Microbiological Testing (Total Aerobic Count, Yeast/Mold, E. coli, Salmonella) prior to QA batch release.
Request Quality Audit DocumentsStrategic B2B Capsule Sourcing & Global Market Trends (2025–2030)
The global dietary supplement industry is undergoing a structural shift driven by consumer demand for transparency, sustainability, and targeted therapeutic performance. Brand managers and global buyers sourcing custom OEM bulk capsules must position their supply chains to capitalize on critical emerging trends over the next decade:
1. The Transition to Clean Label & Excipient-Free Manufacturing
Global regulatory bodies (such as the European Food Safety Authority - EFSA) are tightening rules around traditional additive excipients like Titanium Dioxide (E171) and Magnesium Stearate. Modern brand owners are demanding clean-label capsule formulations that utilize organic rice hulls, tapioca starch, or sunflower lecithin as natural flow agents. Our facility leads the industry in clean-label capsule compounding, achieving rapid machine throughput without relying on synthetic lubricants or artificial colorants.
2. Micro-Pellet & Beadlet-in-Capsule (Multi-Phase Delivery)
Advanced nutritional delivery systems are moving toward multi-phase dosing. By combining oil-filled capsules with encapsulated micro-beadlets, brands can deliver time-released active ingredients in a single transparent visual dosage form. For instance, pairing liquid Omega-3 oil with delayed-release iron or vitamin beadlets prevents nutrient degradation while offering a visually striking product that commands premium retail pricing.
3. Postbiotics, Synbiotics & Spore-Forming Micro-Organisms
Microbiome science has expanded beyond fragile live probiotics toward heat-stable spore-forming strains (such as Bacillus coagulans) and postbiotics. These next-generation ingredients require specialized low-humidity encapsulation environments (RH < 30%) and specialized packaging barriers to guarantee shelf-life activity without refrigeration—a core engineering strength of our factory cleanrooms.
4. Supply Chain Transparency & AI-Driven Batch Traceability
As international supply chains face volatility, enterprise buyers require total visibility from farm to capsule. Our OEM export framework integrates batch-level tracking software, providing complete traceability for botanical harvest origins, extraction solvents, and analytical testing certificates. This documentation stream accelerates customs clearance across major global ports in North America, Europe, Asia-Pacific, and the Middle East.
Why Partner With Our Custom OEM Bulk Capsules Facility?
Choosing an experienced contract manufacturing partner is the single most critical decision for expanding supplement brands. Here is how our enterprise infrastructure delivers superior competitive advantages:
Turnkey OEM / ODM Solutions
From initial concept formulation, flavor masking, and benchtop R&D samples (delivered within 5 business days) to high-speed commercial production, bulk counting, packaging, and custom labeling.
Flexible MOQs & Scalability
Whether launching a pilot line of 5,000 units or scaling to multi-million bulk capsule runs, our tiered pricing structure ensures maximal margin optimization for growing enterprises.
Global Export Logistics
Full export handling including Certificate of Free Sale (CFS), EU Dossiers, Health Certificates, and customized palletization optimized for ocean or air freight container shipping.
Frequently Asked Procurement Questions (FAQ)
Ready to Scale Your Bulk Capsule Manufacturing?
Partner with an industry-leading U.S. cGMP contract manufacturer. Request a custom quote, schedule a facility audit, or speak directly with our formulation engineering team today.
Inquire Now