Industry-Grade Custom Bottles & Rigid Containers
Engineered for high-viscosity cosmetics, luxury fragrances, pharmaceuticals, personal care, and food-grade applications.
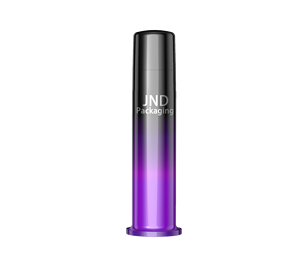
100ml Airless Pump Bottle for High Viscosity Cream Paste All Plastic Dispenser Custom Cosmetic Packaging Set
Send an Inquiry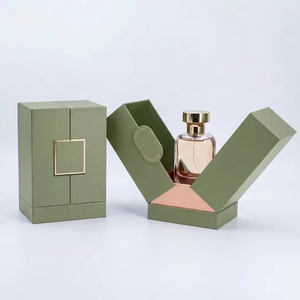
Luxury Double Open Perfume Gift Box Custom Logo Green Cardboard Cosmetic Packaging Box For Perfume Bottle Essential Oil Bottle
Send an Inquiry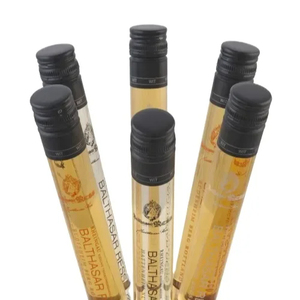
Custom Gift Box Packaging Small Capacity 30ml 50ml 100ml Glass Bottle test Tube Wine
Send an Inquiry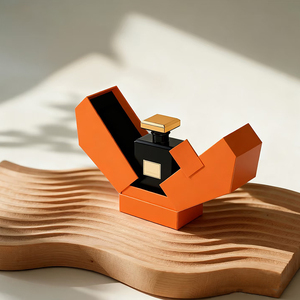
Custom Luxury Rigid Paper Hexagon Perfume Packaging Box Sponge Lining Wholesale High End Fragrance Bottle Gift Box Insert 50ml
Send an Inquiry
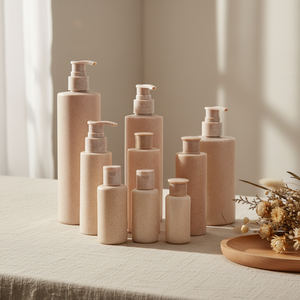
Wholesale Custom Various Size Capacity Logo Press Type Cylindrical Opaque Leak Proof Sealed Airtight PE Plastic Shampoo Bottle
Send an Inquiry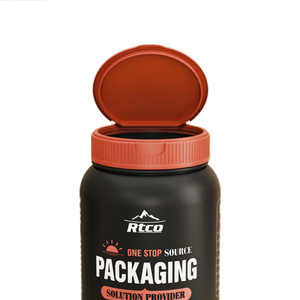
Custom Black 120mm Wide Mouth HDPE Plastic Bottle Packaging with Flip Cap for Collagen Powder
Send an Inquiry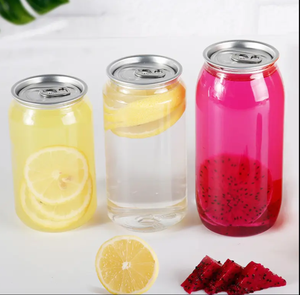
250Ml 350Ml 450Ml 550Ml Custom Transparent Juice Bottle Plastic Drink Cans Seal PET Soda Water Plastic Can For Drink
Send an InquiryState-of-the-Art Manufacturing & Infrastructure
Our advanced industrial plant combines precision mold design, high-speed injection molding, blow molding, and cleanroom packaging under strict cGMP protocols.
Tooling & Rapid DFM
In-house 3D CAD modeling and Moldflow analysis allow 5-day rapid prototyping and high-cavitation production mold creation with tolerances down to ±0.02mm.
Sustainable Polymer Tech
Expertise in processing up to 100% Post-Consumer Recycled (PCR) PET, HDPE, and biodegradable PLA resins, maintaining optical clarity and structural rigidity.
cGMP & ISO Compliance
Every lot undergoes rigorous quality checks: 100% inline camera defect detection, vacuum leak testing, torque tension testing, and heavy metal screen assays.
Turnkey Global Supply
End-to-end management spanning custom surface decorations (silk-screening, hot stamping, UV coating), secondary luxury box packaging, and FOB/DDP export logistics.
2026–2030 Global Bottle Packaging Sourcing Trends
Key economic, environmental, and technological shifts transforming the international contract packaging landscape.
1. Decarbonization & Mandatory PCR Mandates
Global consumer packaging brands are aggressively shifting from virgin fossil-fuel polymers to PCR (Post-Consumer Recycled) resin formulations. Driven by EU packaging directives and US state-level EPR (Extended Producer Responsibility) regulations, procurement strategies prioritize suppliers capable of delivering up to 100% PCR PET and HDPE bottles without compromising mechanical strength or seal integrity.
Chinese top-tier factories are scaling up direct partnerships with certified post-consumer recyclers, providing verified carbon footprint certifications and GRS (Global Recycled Standard) traceability for international compliance.
2. Monomaterial & Eco-Engineered Dispensing
Traditional lotion pumps rely on complex multi-material assemblies, including internal stainless-steel springs and glass ball valves, rendering them non-recyclable in standard municipal waste streams. The market is rapidly transitioning toward 100% All-Plastic Monomaterial Airless Systems.
By engineering plastic springs (using PE or PP polymers) directly into the pump engine, modern packaging manufacturers ensure that the entire bottle unit can be directly tossed into single-stream recycling bins without pre-disassembly.
3. Lightweighting & Structural Optimization
Rising international freight costs and aggressive Scope 3 emissions targets have made light-weighting a priority in bottle structural design. Utilizing high-end Finite Element Analysis (FEA) and multi-layer stretch blow molding techniques, manufacturers can reduce raw material usage by 15% to 25% while retaining top-load strength and drop impact resistance.
This optimization delivers substantial savings in freight weight and raw material expenditures over large volume procurement runs.
Packaging Engineering & Material Science Advancements
In-depth structural breakdown of barrier protection, dispensing dynamics, and polymer compatibility.
High-Viscosity Dispensing & Airless Chemistry
Airless pump technology operates via a mechanical vacuum piston mechanism rather than a traditional dip tube. As the actuator is pressed, it creates a pressure differential that moves an internal disc bottom upward, dispensing exact doses (e.g., 0.2cc to 1.0cc) without introducing ambient air into the reservoir.
- Preservative Reduction: Protects active ingredients (Vitamin C, Retinol, organic botanicals) from oxidation, extending shelf life by up to 150%.
- Near-Zero Evacuation Waste: Achieves >98% product restitution, preventing high-cost cosmetic formulations from remaining trapped inside walls.
- Viscosity Range Handling: Formulated for formulations ranging from 1,000 cP to over 100,000 cP (heavy pastes, body creams, and silicones).
Multi-Layer Co-Extrusion & EVOH Barriers
For chemical, industrial, and high-performance cosmetic formulations sensitive to gas permeation, single-layer HDPE or PET containers are often insufficient. Chinese leading manufacturers utilize multi-layer extrusion blow molding (up to 6 layers) incorporating EVOH (Ethylene Vinyl Alcohol) barrier cores.
This multi-layer technology prevents essential oils, organic solvents, and volatile fragrance compounds from leaching through the container walls while completely blocking oxygen ingress.
| Material / Container System | Key Performance Characteristics | Ideal Application Sectors | Recyclability & Sustainability Profile |
|---|---|---|---|
| All-Plastic Airless Systems (PP/PE) | 100% oxidation barrier, zero metal parts, accurate dose output (0.2–0.5ml). | Luxury Serums, Dermatological Creams, Active Skincare. | 100% Recyclable (RIC 5 / RIC 2), Available in up to 100% PCR. |
| Pharmaceutical Glass (Type I/III) | Impermeable barrier, zero chemical leaching, high thermal resistance. | Essential Oils, Perfumes, Ampoules, Premium Spirits. | Infinitely Recyclable, High Aesthetic Premium Weight. |
| High-Density Polyethylene (HDPE) | High impact strength, excellent chemical/acid resistance, flexible rigid walls. | Shampoos, Chemical Liquids, Nutraceutical Powders. | Highly Recyclable (RIC 2), Widespread Municipal Collection. |
| PET & rPET Drinks / Cans | High optical clarity, shatterproof, lightweight, gas sealable caps. | Beverages, Cold Brews, Juices, Functional Drinks. | 100% Recyclable (RIC 1), Lowest Carbon Shipping Footprint. |
Frequently Asked Sourcing & Manufacturing Questions
Clear, direct answers for B2B procurement managers, brand founders, and supply chain directors.
What are the standard Minimum Order Quantities (MOQs) for custom bottle production?
For standard stock bottles in default colors (white, clear, amber), MOQs typically start at 5,000 to 10,000 units. For fully customized color matching (Pantone PMS), custom surface decorations, or specialized PCR material blends, standard MOQs range from 10,000 to 20,000 units depending on machine cavity sizes.
What is the typical lead time for custom mold tooling and mass production?
Custom mold design, DFM optimization, and 3D prototype sampling generally take 7 to 10 working days. Once pilot samples are approved, steel/aluminum mass production tooling requires approximately 25 to 30 days. Standard turnkey production runs then take 3 to 4 weeks upon raw material clearance.
How do China bottle packaging factories ensure leak-proof performance and quality assurance?
Quality assurance follows strict ISO 9001 and cGMP workflows. Every production lot undergoes vacuum chamber leak testing (-0.08MPa for 15 minutes), drop impact tests from 1.2 meters, neck thread dimensional verification via digital calipers, and automatic inline optical camera detection for flash, bubble, or color contamination defects.
Can you supply food-grade and pharmaceutical-compliant packaging certificates?
Yes. All food, beverage, supplement, and cosmetic packaging products comply with international regulatory frameworks. Factories provide FDA food-contact compliance declarations, EU No 10/2011 material compliance statements, BPA-Free certificates, heavy metal test reports (REACH/RoHS), and GRS certification for recycled plastics.
What surface decoration techniques are available for brand customization?
We offer comprehensive decoration capabilities including high-speed silk-screen printing, hot foil stamping (gold, silver, holographic), UV gradient spraying, soft-touch matte finishes, electroplating, water transfer printing, and custom embossed/debossed logos molded directly into the container structure.
How is product compatibility verified prior to full mass manufacturing?
We strongly recommend compatibility testing. We supply free pre-production samples for client lab testing, including 45°C/60-day accelerated stability oven testing, freeze-thaw cycle testing, and active formula chemical compatibility testing to verify no stress cracking, formula degradation, or liner swelling occurs.
Transform Your Product Packaging Strategy Today
Partner with China's leading bottle packaging manufacturer. Gain direct access to custom mold engineering, certified sustainable materials, competitive factory-direct pricing, and world-class quality control.