Precision-Formulated Dietary & Vitamin Products
Turnkey OEM/ODM Contract Manufacturing Solutions Built on Automated Processing & International Compliance
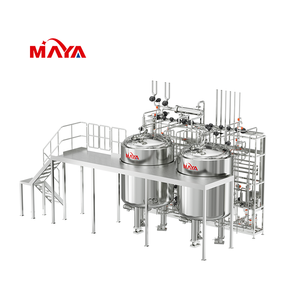
Marya China Manufacturer Customized Fully Automated Formulation System
Contact Us
OEM ODM Custom Formulation Cassia Seed Extract 10:1 Botanical Powder
Contact Us
Private Label Creatine Monohydrate Powder Bulk Sports Nutrition
Contact Us
Private Label L-Carnitine Taurine Energy Powder Custom Formulation
Contact Us
Triple Omega 3-6-9 Softgel Capsules EPA DHA Cardiovascular Support
Contact Us
Plant-Based Organic Protein Powder Custom Formulation Bulk Supply
Contact Us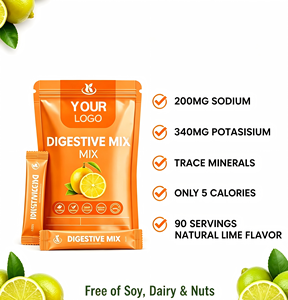
Custom Hydration Electrolyte Powder Private Label GMP Certified
Contact Us
Multi-Species Mineral Premix Animal Nutrition Feed Additives
Contact Us1. Technical Whitepaper: The Paradigm Shift in CE Certified Vitamin Manufacturing
The global nutraceutical, dietary supplement, and specialized vitamin manufacturing sectors are undergoing a structural transformation. Brand owners, clinical nutrition firms, and institutional procurement networks no longer evaluate manufacturing partners solely on unit-cost metrics. Modern market dynamics, driven by stringent cross-border regulatory frameworks and heightened consumer scrutiny, demand absolute analytical transparency, robust validation engineering, and seamless compliance alignment across international jurisdictions.
Historically, the CE Marking (Conformité Européenne) was associated predominantly with medical devices, electrical machinery, and industrial hardware within the European Economic Area (EEA). However, in modern advanced nutraceutical production, the concept of a "CE Certified Vitamin Manufacturing Factory" represents a sophisticated synthesis between automated industrial processing equipment compliance (Directives 2006/42/EC and 2014/35/EU) and strict international Good Manufacturing Practices (cGMP, NSF, ISO 22000, and FDA 21 CFR Part 111).
| Compliance Architecture | Regulatory Framework / Directive | Impact on Vitamin Manufacturing Quality |
|---|---|---|
| CE Machinery Directive | Directive 2006/42/EC | Ensures automated dosing, mixing, and encapsulation lines operate under strict error-proof mechanical precision, preventing batch contamination. |
| cGMP Dietary Supplements | FDA 21 CFR Part 111 / NSF/ANSI 173 | Governs raw material identity verification, active assay overages, in-process weight uniformity, and finished product potency validation. |
| EU Food Supplement Directive | Directive 2002/46/EC | Regulates approved vitamin/mineral chemical forms, bio-availability benchmarks, and maximum safe upper intake limits (UL). |
| Automated Formulation Traceability | FDA 21 CFR Part 11 / Annex 11 | Guarantees electronic batch record integrity, audit trails, and automated sensor data logging across high-speed packaging lines. |
When procuring from a facility equipped with high-precision customized fully automated formulation systems (such as specialized Marya automated lines), enterprise buyers gain an unmatched competitive advantage: batch-to-batch coefficient of variation (CV) held under 1.5%, zero cross-contamination risks due to closed-loop pneumatic transfer, and full digital batch execution logs downloadable for instant regulatory clearance.
2. Enterprise Technological Superiority & Facilities Architecture
At the core of premier contract manufacturing lies physical infrastructure engineered specifically to control atmospheric environmental variables. Maintaining micro-nutrient integrity—specifically sensitive water-soluble vitamins (such as Vitamin C, B-complex) and fat-soluble carotenoids/lipids—requires strict control over relative humidity (RH), temperature, UV spectrum exposure, and airborne particulates.
17 Independent Cleanrooms
Separate positive and negative air pressure HVAC zones prevent airborne cross-contamination between botanical extracts, allergen proteins, and micro-dose vitamin premixes.
Automated Dosing Precision
Integrated loss-in-weight gravimetric feeders ensure active botanical extracts (e.g., Cassia Seed 10:1) and concentrated vitamins are uniformly distributed in macro-blends.
Analytical QA / QC Testing
Every single batch undergoes HPLC assay testing for active vitamin potency, ICP-MS for heavy metals (Lead, Cadmium, Arsenic, Mercury), and complete USP microbial screening.
Comprehensive Material Flow & Processing Hygiene
Modern vitamin synthesis and formulation require strict separation between raw material receiving, quarantine sampling, automated dispensing, blending, dosage delivery (encapsulation/tableting/powder filling), and primary packaging. Utilizing standardized cleanroom modular architecture allows our facilities to deliver pharmaceutical-level cleanliness across high-volume commercial runs.
- Low-Humidity Encapsulation Suites: Maintained under 30% RH for hygroscopic formulations including amino acid complexes (L-Carnitine, Taurine) and effervescent electrolyte matrices.
- Softgel Encapsulation & Drying Tunnels: Controlled temperature and humidity zones for lipid-based delivery vehicles like Triple Omega 3-6-9, optimizing gelatin/pectin shell elasticity and oxidative stability.
- High-Velocity Powder Blending: V-Blenders and Ribbon Mixers equipped with liquid injection bars for micro-encapsulated vitamin spraying, ensuring perfect homogeneity.
3. Global Vitamin Sourcing & Procurement Trends (2026–2030)
As global supply chains normalize post-disruption, B2B nutraceutical buyers, private label brands, and pharmacy chains are shifting their procurement strategies toward high-yield, verified, resilient partners. Procurement leaders who want to maintain margin integrity while capturing market share must navigate four critical industry megatrends:
A. Transition to Micro-Encapsulation & Liposomal Delivery Systems
Standard ascorbic acid, un-complexed Vitamin D3, and traditional B-vitamins face degradation when exposed to gastric acid. The market is shifting toward liposomal and micro-encapsulated formulations that bypass harsh stomach acid to deliver superior intestinal absorption. Manufacturing factories capable of handling beadlet technology and oil-in-water nano-emulsions are capturing the premium retail segment.
B. Clean-Label, Plant-Based Excipient Replacement
Global consumers actively reject synthetic flow agents like magnesium stearate, silicon dioxide, and artificial colorants. Future-proof factories have re-engineered their blending dynamics to utilize organic rice hulls, tapioca maltodextrin, and natural botanical colorants without sacrificing tableting hardness or capsule filling speeds.
C. High-Functional Multi-Ingredient Synergies
Single-ingredient vitamins are rapidly giving way to complex, target-driven wellness stacks. High-growth product categories include:
- Metabolic & Weight Management Stacks: Combining L-Carnitine, Taurine, and botanical extracts like Cassia Seed with B-vitamin co-factors for cellular energy yield.
- Cardiovascular Lipid Matrixes: Blending Triple Omega 3-6-9 (EPA/DHA/GLA) with CoQ10 and Vitamin K2 (MK-7) to preserve arterial elasticity and cognitive health.
- Hydration & Performance Electrolytes: Low-carb, sugar-free electrolyte powders enriched with ionic trace minerals, Vitamin C, and bioflavonoids for rapid cellular rehydration.
- Pet & Animal Wellness Additives: Specialized trace mineral premixes and animal-grade vitamin fortifiers designed for targeted companion animal and livestock nutrition.
D. Automated Regulatory Documentation & Digital Compliance Clearance
Cross-border customs inspections and e-commerce platform compliance (such as Amazon Seller Central Requirements for Dietary Supplements) now require instant submission of verified Certificates of Analysis (CoA), ISO 17025 accredited laboratory assay data, stability reports, and raw material origin traceability. Factories integrated with digital automated batch control offer zero-delay clearance for global shipments.
4. OEM/ODM Dosage Form Technical Capabilities Matrix
Our factory infrastructure supports a multi-dimensional range of finished product dosage forms, engineered to meet exact client specifications and consumer delivery preferences:
| Dosage Format | Technical Capabilities & Specifications | Ideal Product Applications |
|---|---|---|
| Two-Piece Capsules | Gelatin & HPMC Vegetable Shells (Sizes 000 to 4); Delayed-release enteric coating; Banded capsules. | Single/Multi-Vitamin mixes, Botanical Extracts (Cassia Seed), Thermogenic Energizers. |
| Lipid Softgels | Oval, Oblong, Round shapes; Custom gelatin/pectin shell clarity; Nitrogen-blanketed filling. | Triple Omega 3-6-9, Vitamin D3/K2, CoQ10, Liposomal Vitamin E solutions. |
| Powders & Stick Packs | 5,000+ kg batch blending; High-speed sachet & jar filling; Instantized water-soluble milling. | Creatine Monohydrate, Plant Proteins, L-Carnitine Taurine Mixes, Electrolytes. |
| Compressed Tablets | Chewable, Effervescent, Sublingual, and Bi-Layer tablets; Custom embossing and film coating. | Daily Multivitamins, High-Potency Vitamin C, Mineral Premixes, Animal Supplements. |
5. Enterprise Sourcing & Manufacturing FAQ
Key technical and procurement answers for brand managers, regulatory specialists, and supply chain directors:
Partner with a World-Class CE & cGMP Certified Manufacturer
Scale your nutraceutical product pipeline with automated precision, absolute regulatory compliance, and market-ready custom formulations. Contact our engineering and procurement team today for a comprehensive feasibility evaluation.
Contact Us