Featured CE & cGMP Compliant Protein & Supplement Solutions
Direct from certified manufacturing lines: Turnkey formulation, bulk powder blending, custom encapsulation, and private-label sports nutrition engineered for global export.
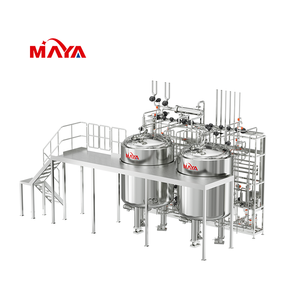
Marya China Manufacturer Customized Fully Automated Formulation System
Get Catalog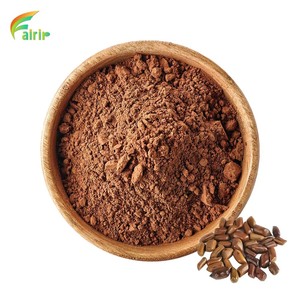
OEM ODM Custom Formulation Cassia Seed Extract 10:1 Food Grade Powder
Get Catalog
Private Label Custom Formulation Creatine Monohydrate Powder Wholesale
Get Catalog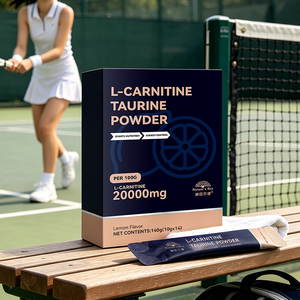
Private Label L-Carnitine Taurine Energy Powder Blend
Get Catalog
Triple Omega 369 Softgel Capsules Cardiovascular Support
Get Catalog
Private Label Plant-Based Protein Powder Custom Formulation
Get Catalog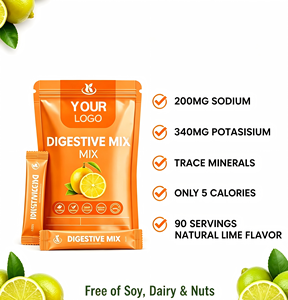
Custom Electrolyte Hydration Powder Supplement Low Carb
Get Catalog
Multi-Species Mineral Premix for Animal Nutrition Feed Additive
Get CatalogThe Technical & Regulatory Framework of CE Certified Protein Manufacturing
Navigating European Conformity, Food Safety Directives, and Advanced Bio-Manufacturing Standards for Global Sourcing Operations
Regulatory Standard Compliance & CE Marking Requirements
In the modern international contract manufacturing ecosystem, sourcing protein powders, functional nutritional premixes, and dietary supplements requires rigorous adherence to European Directive standards. Obtaining CE certification alongside NSF cGMP registration guarantees that processing machinery, cleanroom air sanitation systems, automated filling lines, and end-product matrixes comply with essential European Health, Safety, and Environmental Protection standards (EC 178/2002 and Regulation EC 852/2004).
Quality Risk Management (QRM) & Hazard Analysis
High-tier protein manufacturing facilities implement robust HACCP (Hazard Analysis Critical Control Point) protocols integrated directly into SCADA-controlled automated formulation systems. From raw material intake through ultrafiltration, spray-drying, and pneumatic conveyance to final primary packaging, every critical control point is monitored to eliminate cross-contamination, botanical adulteration, heavy metal ingress, and microbiological proliferation.
"Information Gain Insights: Sourcing protein and supplement powders from a manufacturer equipped with integrated automated cleanroom lines reduces batch-to-batch coefficient of variation (CV) to under 1.2%, significantly lowering regulatory rejection rates at European and North American customs border controls."
Automated Processing Facilities & Production Engineering
Integrating state-of-the-art pharmaceutical-grade processing equipment with scalable OEM/ODM capabilities.
Fully Automated Formulation Systems
Our strategic production lines leverage continuous gravimetric micro-dosing systems and liquid formulation skid systems (such as customized Marya automation platforms). This guarantees micro-nutrient, vitamin, and trace mineral distribution accuracy within ±0.1% across multi-ton protein powder batches.
ISO Class 7 Cleanroom Air Filtration
Blending and primary filling operations occur inside positive-pressure cleanroom suites featuring HEPA air filtration (99.97% efficiency at 0.3 microns). Differential pressure zones isolate botanical extraction rooms, probiotic handling environments, and dairy/plant protein blending suites to maintain complete allergen separation.
Advanced Particle Engineering & Spray Drying
Utilizing low-temperature spray drying and fluid-bed agglomeration technology, we transform non-instantized plant proteins (pea, rice, pumpkin seed) and whey hydrolysates into free-flowing, instantized powders with superior dispersion metrics in cold liquids.
Protein & Supplement Manufacturing Technical Specifications Matrix
Comprehensive analytical parameters for factory sourcing and quality assurance evaluation.
| Dosage / Product Format | Core Ingredients & Matrix options | Processing & Packaging Technology | Quality & Regulatory Certifications |
|---|---|---|---|
| Plant-Based Protein Powders | Pea Protein Isolate, Organic Rice Protein, Pumpkin Seed, Fava Bean, Bioactive Enzymes | Fluid-Bed Instantization, Nitrogen Flushing, High-Barrier Composite Containers / Pouches | CE Mark, NSF cGMP, USDA Organic, ISO 22000, Non-GMO Project Verified |
| Sports Nutrition Blends | Micronized Creatine Monohydrate, L-Carnitine Tartrate, Taurine, BCAA 2:1:1, Electrolytes | High-Shear Dry Blending, Gravimetric Powder Filling, Induction Sealed Closure | CE Compliant Lines, WADA Banned Substance Tested, Halal & Kosher Options |
| Nutraceutical Softgels | Triple Omega 3-6-9, Concentrated Fish Oil (EPA/DHA), Evening Primrose Oil, Phytosterols | Rotary Die Encapsulation, Low-Humidity Drying Tunnels, Blister / HDPE Bottle Packaging | FDA Registered, Friend of the Sea Certified, Heavy Metal Free (ICP-MS Tested) |
| Functional Botanical Extracts | Cassia Seed Extract (10:1), Green Tea EGCG, Ashwagandha, Perilla Seed Extract | Counter-Current Hydro-Ethanolic Extraction, Vacuum Concentration, Spray Drying | CE Certified Extraction Plant, ISO 9001, HPLC Potency Standardized |
Future Procurement & Manufacturing Trends (2025–2030)
Key shifts impacting global protein sourcing, contract manufacturing specifications, and clean-label compliance.
Precision Bio-Fermentation & Recombinant Proteins
The global market is rapidly transitioning beyond traditional animal hydrolysates toward precision-fermented proteins. Contract manufacturers with specialized stainless-steel bioreactors can produce identical whey and collagen peptide sequences without animal inputs, satisfying strict European sustainability directives.
Ultra-Clean Label & Synthetic Emulsifier Elimination
Importers are demanding the removal of synthetic anti-caking agents (such as silicon dioxide) and artificial emulsifiers (carboxymethyl cellulose). Modern factories now employ enzymatic lecithination and natural bamboo/sunflower fiber systems to maintain instant solubility.
Bioactive Peptide Isolation & Targeted Health Claims
Rather than selling commodity macro-protein, top exporters are focusing on enzymatic cleavage technologies that yield specific molecular weight bioactive peptides (under 1,000 Daltons) for targeted cardiovascular, muscle recovery, and glucose modulation benefits.
Smart Supply Chain Traceability & Blockchain Lot Code Integration
Regulatory bodies require granular farm-to-tub transparency. Fully automated packaging lines now laser-engrave unique QR lot identifier codes on tub bottoms, allowing retailers and consumers to view third-party Certificate of Analysis (CoA) records instantly.
Global Export Documentation & Analytical Testing Protocols
Ensuring full compliance with US FDA, EU EFSA, and international customs entry standards.
Microbiological & Pathogen Screening
Every finished batch undergoes rigorous testing via Rapid PCR and USP <2021>/<2022> protocols for Total Aerobic Microbial Count (TAMC), Yeast & Mold, E. coli, Salmonella spp., and Staphylococcus aureus before inventory release.
Heavy Metals & Elemental Analysis
Utilizing Inductively Coupled Plasma Mass Spectrometry (ICP-MS), we verify that lead, cadmium, mercury, and arsenic levels meet stringent EU limits under Regulation (EC) 1881/2006 and California Proposition 65 thresholds.
Potency & Amino Acid Profile Validation
High-Performance Liquid Chromatography (HPLC) and High-Speed Amino Acid Analyzers quantify exact active levels—guaranteeing that label claims for leucine, isoleucine, valine, creatine, L-carnitine, and botanical bio-actives are 100% verified.
Frequently Asked Questions for Protein Buyers & Importers
Direct answers to common questions about CE certification, OEM minimum order quantities, and contract manufacturing logistics.
Q: What does CE certification signify for a protein manufacturing facility?
CE certification confirms that the manufacturing plant's automated machinery, electrical control units, steam sterilization vessels, and cleanroom air systems satisfy mandatory European Union Directive requirements (including the Machinery Directive 2006/42/EC and Electromagnetic Compatibility Directive 2014/30/EU). For global brand owners, sourcing from a CE-marked facility ensures high engineering standards, operational safety, and conformity with European food processing equipment regulations.
Q: What are the standard Minimum Order Quantities (MOQs) for custom formulations?
For ready-to-label private-label formulations (powder or capsules), standard MOQs typically start at 5,000 units. Fully customized formulations—requiring specific flavor development, unique plant-protein blends, or custom active pre-mixes—generally start at 10,000 units or 1,000 kg total powder batch yield. Volume tiered pricing is available for production runs of 25,000, 50,000, and 100,000+ units.
Q: How do you ensure flavor stability and mask off-notes in plant-based proteins?
Our in-house R&D application scientists utilize proprietary micro-encapsulation and natural flavor masking systems. By encapsulating astringent botanical tannins or earthy notes in vegan pea/rice proteins, we achieve clean organoleptic profiles. Flavor stability is validated through real-time and accelerated thermal stability chamber testing (40°C / 75% Relative Humidity).
Q: Can your factory assist with Amazon Seller Central and EU import documentation?
Yes. We provide complete compliance dossiers for every order. This includes lot-specific Certificates of Analysis (CoA), cGMP facility certificates, ISO 22000 documentation, full Allergen Statements, Non-GMO declarations, Stability Reports, and BSE/TSE-Free Certificates required by customs authorities and retail platforms worldwide.
Q: What are the lead times for custom OEM/ODM production runs?
Standard lead times follow a structured workflow: Quotation and formulation feasibility assessment: 48 hours. R&D pilot batch sampling and flavor sign-off: 5–7 business days. Commercial production, analytical testing, and final quality release: approximately 6–8 weeks following packaging artwork approval and raw material staging.
Q: How do you manage allergen cross-contamination between dairy and vegan products?
We enforce strict allergen control procedures in accordance with cGMP 21 CFR Part 111. Dairy proteins (whey, casein) and plant-based/vegan lines are manufactured in physically separated cleanroom suites. Between production shifts, automated Clean-In-Place (CIP) systems sanitize stainless steel blenders and pneumatic pipelines, followed by swab validation testing (ELISA) for milk protein residue.