Turnkey Encapsulation & Custom Formulation Portfolio
Exceeding European CE Machinery Safety Directives and US FDA cGMP standards. High-potency, stable dosage manufacturing engineered for maximum bioavailability.
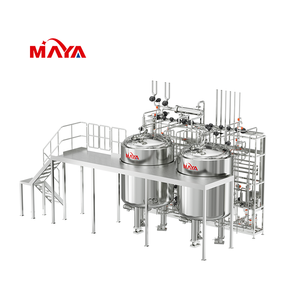
Automated Bulk Formulation System
Custom engineered liquid, powder, and micro-pellet automated compounding system ensuring strict cross-contamination controls for high-throughput lines.
Get Catalog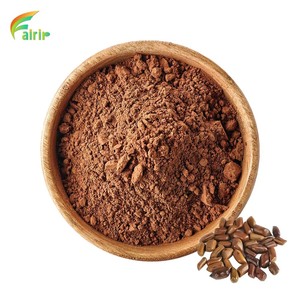
Botanical Extract Encapsulation Grade
10:1 Cassia Seed Extract standardized botanical bulk powder designed for optimal capsule flowability, moisture stability, and enteric release profiles.
Get Catalog
Micronized Creatine Monohydrate
Ultra-pure micronized sports nutrition powder engineered for rapid hard-shell capsule encapsulation without dusting or weight variation issues.
Get Catalog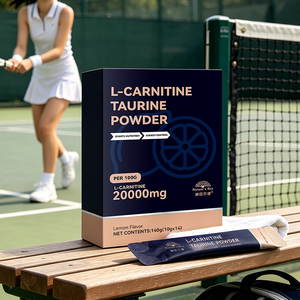
L-Carnitine + Taurine Matrix
Synergistic metabolic support energy formulation available in hygroscopic-protected HPMC capsule shells or travel-ready stick pack formats.
Get Catalog
Triple Omega 3-6-9 Softgels
High-potency EPA/DHA softgel capsules with nitrogen-flushed oxidation protection for cardiovascular, brain, and joint anti-inflammatory health positioning.
Get Catalog
Plant-Based Protein & Aminos
Custom OEM organic pea and brown rice protein matrices available in bulk, powder tubs, or encapsulated precise post-workout dosing options.
Get Catalog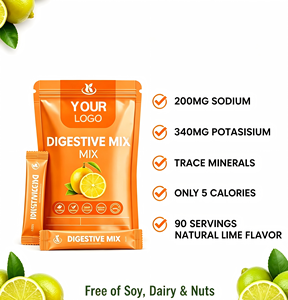
Low-Carb Electrolyte Hydration
GMP-certified trace mineral complex with high bio-absorbability, formulated to prevent clumping during high-speed automated capsule filling.
Get Catalog
Multi-Species Mineral Premix
Veterinary-grade trace mineral feed premix and specialized animal health capsule supplements manufactured under strict biosecurity protocols.
Get CatalogIndustrial Encapsulation Technology & CE Compliance Standards
Understanding the precision engineering, pharmaceutical mechanical standards, and quality validation behind high-speed capsule filling manufacturing.
CE Machinery Certification
Our automated capsule filling machinery fully complies with European Health, Safety, and Environmental Protection standards (Directives 2006/42/EC). Built with 316L contact-grade stainless steel, integrated interlock safety systems, and electro-magnetic compatibility (EMC) for continuous 24/7 commercial operation.
- Fully compliant with EU Machinery Directive 2006/42/EC
- Stainless steel 316L product contact zones
- Failsafe emergency shutoffs & pressure sensors
Precision Tamping & Dosing
Engineered with multi-stage tamping pin technology that compresses powders into dense slugs with minimal shear stress. This guarantees fill weight variation within ±1.5%, even for difficult, non-free-flowing botanical powders, hygroscopic extracts, and micro-encapsulated lipids.
- 5-stage tamping pin compression technology
- Handles sizes 000, 00, 0, 1, 2, 3, and 4
- Automatic weight correction via closed-loop feedback
Cleanroom & HVAC Integration
Manufacturing occurs inside 17 independent, positive-pressure cleanrooms equipped with HEPA filtration (ISO Class 7 / Grade C equivalent). Humidity is strictly controlled under 30% RH for moisture-sensitive formulations like probiotics and effervescent salts.
- ISO Class 7 cleanroom environment
- Dehumidified production zones (<30% RH)
- Complete cross-contamination prevention
Information Gain Index: Bioavailability & PowderRheology Engineering
A critical challenge in contract encapsulation is raw material flowability—measured by Carr’s Index and Hausner Ratio. Poorly flowing botanical extracts often lead to weight variation and erratic dosage uniformity. Enova Science resolves this at the particle level by employing fluid-bed micro-granulation and direct-compression excipient balancing. This process converts cohesive herbal powders into free-flowing granules, maximizing capsule yield and maintaining tight analytical potency claims batch after batch.
Single-Source OEM/ODM Manufacturing Excellence
From raw material qualification to automated bottle filling and blister packaging, our Fort Myers, Florida facility simplifies complex supply chains.
Complete Polymer Versatility
Whether your brand requires standard Bovine Gelatin, Kosher/Halal certified formulations, Plant-Derived HPMC (Hydroxypropyl Methylcellulose) for clean-label claims, or acid-resistant Enteric capsules for intestinal probiotic delivery, our filling lines seamlessly run all shell variants.
Rigorous Batch Documentation
Every commercial lot is accompanied by a Master Batch Record (MBR), full raw material identity verification via FTIR testing, weight variation audit logs, disintegration testing profiles (USP <2040>), and finished-product Certificates of Analysis (CoA).
Amazon & International Compliance
Selling on Amazon Seller Central or exporting to EU, Asian, and Latin American markets requires strict analytical proof. We deliver standard heavy metal screens (ICP-MS), microbial limit testing (USP <2021/2022>), solvent residue assays, and allergen-free certifications.
Speed-to-Market Agility
With R&D pilot samples delivered within 5 working days and complete turnkey production runs fulfilled in roughly 8 weeks, our agile supply chain management mitigates stockout risks for rapidly scaling supplement brands.
Capsule Shell Polymer & Fill Material Compatibility
Selecting the ideal combination of capsule shell and internal formulation phase to optimize active delivery, shelf-life stability, and consumer compliance.
| Capsule Type | Material Origin | Ideal Formulation Phase | Moisture Sensitivity | Dissolution Target Zone |
|---|---|---|---|---|
| Gelatin (Standard) | Porcine / Bovine Collagen | Dry Powders, Non-hygroscopic Minerals | 13% - 16% Content | Immediate Release (Stomach ~15 mins) |
| HPMC (Vegetarian) | Pine Bark / Wood Cellulose | Botanicals, Herbal Extracts, Hygroscopic Actives | 4% - 7% Content (Low) | Immediate Release (Stomach ~20 mins) |
| Enteric HPMC | Modified Plant Cellulose | Probiotics, Enzymes, Acid-Sensitive Peptides | Low Water Activity | Targeted Delayed Release (Small Intestine) |
| Liqui-Cap (Hard Gel/HPMC) | Gelatin or HPMC Shell + Banding | Lipophilic Extracts, Omega-3 Oils, Suspensions | Zero Water Tolerance | Rapid Lipid Absorption & Reduced Burp-back |
Future Procurement & Technological Development Trends (2025-2030)
Strategic insights for enterprise procurement officers, supply chain directors, and nutraceutical brand founders.
1. Transition to Titanium Dioxide-Free Capsules
Driven by the European Food Safety Authority (EFSA) ban on E171 (Titanium Dioxide) as a food additive, global brands are rapidly transitioning to clean-label opacifiers. Enova Science offers natural white opacified capsules derived from calcium carbonate and starch derivatives that comply with both EU and US FDA regulations without compromising light barrier protection.
2. Multi-Phase & Combo Encapsulation
Consumers are demanding simplified daily regimens. Future procurement is shifting heavily toward Liquid-Fill Hard Capsules (LFHC) containing suspended beads, micro-tablets, or secondary dual capsules (Cap-in-Cap). This technology allows un-mixable actives—such as water-soluble B-vitamins inside an oil-soluble Omega-3 matrix—to be delivered in a single dose.
3. Real-Time AI Quality Control (PAT Integration)
Traditional batch testing is giving way to Process Analytical Technology (PAT). Next-generation CE-certified capsule filling lines utilize Near-Infrared Spectrometry (NIR) directly inside the dosing disk to monitor powder blend uniformity continuously. This automated feedback loop ejects off-spec capsules in micro-seconds, ensuring 100% batch integrity.
Frequently Asked Questions for B2B Encapsulation & Export
Clear, authoritative answers regarding technical specifications, minimum order quantities, compliance documentation, and global shipping logistics.
What minimum order quantities (MOQs) do you require for custom capsule filling?
For ready-to-brand stock private label capsule formulas, our MOQ starts at 5,000 bottles (or bulk equivalent). For custom client-specified formulations requiring specialized raw material procurement, micro-pelletized ingredients, or custom-printed capsule shells, standard production runs typically start at 10,000 to 50,000 units, with substantial volume discount pricing tiers at 100,000+ units.
How does your factory ensure compliance with European CE Directives?
All high-speed encapsulation equipment utilized in our facility undergoes rigorous CE safety evaluation and compliance testing. This encompasses mechanical risk assessments under Directive 2006/42/EC, electrical safety under Low Voltage Directive 2014/35/EU, and electromagnetic shielding. These standards guarantee operational stability, zero metallic micro-particle shedding, and consistent production speed.
Can you handle highly hygroscopic or heat-sensitive herbal extracts?
Yes. Our facility features 17 environmentally controlled production rooms equipped with independent HVAC systems capable of maintaining relative humidity (RH) below 30% and ambient temperatures under 20°C. Furthermore, we can utilize low-moisture HPMC capsule shells (4-7% moisture content compared to 13-16% in standard gelatin) to prevent moisture transfer and capsule softening.
What analytical testing documentation is supplied with international export shipments?
Every batch released from our facility includes a full, comprehensive Certificate of Analysis (CoA) generated by our ISO 17025 accredited laboratory partners. Deliverables include Assay & Potency verification for active markers, Heavy Metal limits (Lead, Cadmium, Arsenic, Mercury via ICP-MS), Microbial Analysis (Total Plate Count, Yeast & Mold, E. coli, Salmonella), Disintegration time verification, and Allergen/GMO-free statements.
Do you assist with Amazon Seller Central documentation requirements?
Absolutely. Amazon requires dietary supplement sellers to submit COAs from ISO/IEC 17025 accredited laboratories, evidence of cGMP facility registration, and finished product imagery displaying matching lot numbers. We provide complete compliance dossier packages specifically formatted for immediate Amazon Seller Central approval.
What is the standard turnaround time from contract signing to final product delivery?
Initial R&D pilot samples and lab trial batches are completed within 5 business days. Once formulation, sample testing, and packaging artwork are approved, standard commercial production runs take approximately 8 weeks. This timeline covers raw material quarantine/testing, encapsulation, bottle/blister packaging, final QA release, and freight loading.
Scale Your Supplement Brand With A CE-Certified Contract Manufacturer
Whether you require custom botanical encapsulation, plant-based HPMC formulas, or high-volume private label supply, our engineering and R&D teams are ready to execute your formulation goals.
Get Catalog